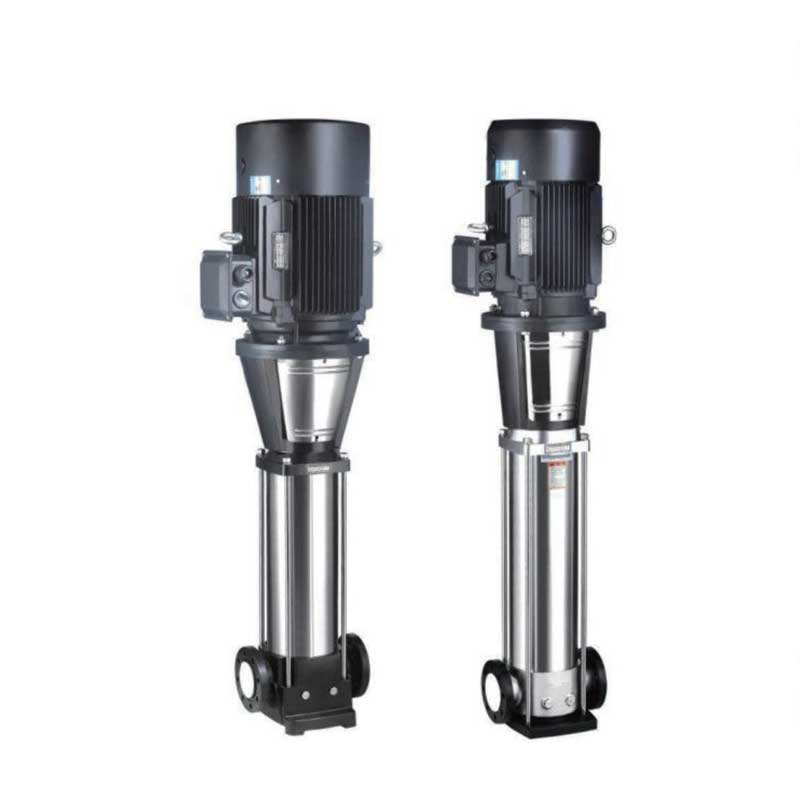
Discover the Efficiency of Single Stage Single Suction Chemical Pumps
Title: Revolutionizing Chemical Pumping: Single Stage Single Suction Pumps Set to Redefine Industry Standards Introduction: Chemical pumps are an integral part of industries that deal with the safe transfer of hazardous and corrosive substances. To ensure efficiency and reliability, leading manufacturers are constantly developing innovative solutions. One such groundbreaking technology is the Single Stage Single Suction Chemical Pump, designed to address various challenges faced by different industries across the globe. In this article, we will explore the features, benefits, and potential applications of this revolutionary pump, highlighting its role in meeting industrial demands and safeguarding productivity. 1. Unraveling the Single Stage Single Suction Chemical Pump: The Single Stage Single Suction Chemical Pump, a product developed by {Company Name}, is an advanced pumping solution that combines cutting-edge technology with superior performance. With an extensive range of features, this pump promises to transform operations and streamline processes within the chemical industry. The pump's mechanics ensure maximum efficiency by maintaining a single suction point, enabling the creation of a more uniform flow, and reducing energy consumption. Its compact design allows for easy installation in confined spaces, making it a versatile choice for various industrial applications. 2. Enhanced Performance and Durability: Built with precision engineering, this chemical pump boasts excellent durability, ensuring consistent performance even in harsh operating conditions. Its corrosion-resistant materials, coupled with effective sealing mechanisms, protect the pump against chemical abrasion, extending its lifespan and reducing maintenance costs. The pump's streamlined hydraulics enable seamless operation, resulting in reduced downtime and increased productivity. Furthermore, its low vibration and noise levels contribute to a safer and more comfortable working environment for operators. 3. Versatility in Applications: The Single Stage Single Suction Chemical Pump caters to a wide range of chemical transfer needs, making it an ideal choice for diverse industries. Whether it's handling acids, alkalis, corrosive liquids, or even waste treatment processes, this pump tackles the challenges efficiently. Its compatibility with different chemical compositions ensures smooth and reliable operation under varying scenarios. From petrochemical plants to pharmaceutical companies, from paper mills to wastewater treatment plants, this pump finds applications in numerous industrial sectors, contributing to the overall efficiency and safety of operations. 4. Environmentally Conscious Design: Adhering to the principles of sustainability, the Single Stage Single Suction Chemical Pump is designed to minimize environmental impact. Its energy-efficient operation reduces power consumption, resulting in lower carbon emissions and reduced ecological footprints. Additionally, the pump's innovative sealing mechanisms prevent chemical leaks, reducing the risk of contamination and ensuring the safety of employees and the surrounding ecosystem. 5. Future-Ready Technology: The Single Stage Single Suction Chemical Pump represents the future of chemical pumping, driving the industry towards greater efficiency and reliability. As companies strive for continuous improvement, this pump offers the latest advancements in technology, ensuring compatibility with evolving industrial demands. By embracing this innovative solution, companies can stay ahead in a competitive market, keep up with regulatory requirements, and minimize operational risks. Conclusion: The Single Stage Single Suction Chemical Pump, developed by {Company Name}, is revolutionizing the chemical pumping industry with its cutting-edge technology and outstanding performance. Its superior durability, versatility, and environmentally-friendly design make it an ideal choice for various industrial applications. With this remarkable pump, companies can increase operational efficiency, reduce maintenance costs, and ensure a safer working environment. Embracing the Single Stage Single Suction Chemical Pump is a step towards transforming the industry and sustaining long-term success.
Read More
Discover the Latest Breakthrough in Centrifugal Pump Technology
Title: Next-Generation Centrifugal Pump Revolutionizes Industrial ProcessesIntroduction:In a significant leap towards achieving higher efficiency and enhanced performance in industrial processes, company {} recently unveiled its latest innovation - the DN ANSI Centrifugal Pump. This groundbreaking pump promises to revolutionize fluid handling applications across various sectors such as oil and gas, chemical, water treatment, and more. With its cutting-edge design and advanced features, the DN ANSI Centrifugal Pump is poised to become an indispensable asset for industries worldwide.Unparalleled Efficiency and Performance:The DN ANSI Centrifugal Pump is engineered to deliver exceptional efficiency, ensuring optimal energy utilization while minimizing operational costs. Equipped with state-of-the-art technology, it offers enhanced control over the flow rate and head, enabling precise adjustment to match varying process requirements.The pump's unique impeller design, coupled with carefully selected materials, ensures excellent resistance to corrosive substances, making it suitable for handling aggressive fluids in chemical and petrochemical industries. It guarantees sustained performance, even when exposed to demanding operating conditions, contributing to increased productivity and reduced maintenance downtime.Seamless Adaptability and Customizability:The DN ANSI Centrifugal Pump's flexibility allows seamless integration into existing systems with minimal modifications. Its standardized dimensions conform to ANSI (American National Standards Institute) specifications, making replacements and upgrades hassle-free. With the ability to handle a wide range of temperatures, pressures, and viscosities, this pump can be tailored to meet specific project requirements.Furthermore, the DN ANSI Centrifugal Pump offers a range of optional features, including low-flow recirculation, double seals, and various impeller configurations. This adaptability enables end-users to optimize their operations and achieve greater process control, ultimately leading to improved product quality and reduced wastage.Advanced Monitoring and Remote Control capabilities:The incorporation of advanced IoT (Internet of Things) technology allows for seamless remote monitoring and control over the DN ANSI Centrifugal Pump. Real-time performance data, including key parameters such as temperature and vibration, are continuously transmitted, enabling operators to remotely track the pump's health, identify potential issues, and take necessary corrective actions promptly. This feature significantly contributes to preventing critical failures, minimizing unplanned downtime, and optimizing system performance.Sustainable Design and Energy Efficiency:{} consistently places emphasis on environmental responsibility, and the DN ANSI Centrifugal Pump is no exception. Its innovative design incorporates energy-efficient features, resulting in reduced power consumption and carbon footprint. This eco-friendly pump aligns with contemporary sustainability goals and regulations, supporting the overall reduction of operational costs and environmental impact.Future Prospects and Commitment to Excellence:With its remarkable efficiency, adaptability, and advanced features, the DN ANSI Centrifugal Pump by {} represents a paradigm shift in industrial fluid handling applications. It is poised to usher in a new era of enhanced productivity, reduced downtime, and optimized resource utilization across various sectors.As a renowned industry leader, {} has always been dedicated to providing cutting-edge solutions to meet its clients' evolving needs. The DN ANSI Centrifugal Pump is a testament to their commitment to technological innovation and delivering top-tier products and services.Conclusion:The introduction of the DN ANSI Centrifugal Pump marks a significant milestone in the industrial fluid handling sector. By harnessing the latest technological advancements, this groundbreaking pump promises unrivaled efficiency, adaptability, and performance. With its potential to revolutionize industrial processes globally, the DN ANSI Centrifugal Pump stands at the forefront of innovation, contributing to sustainable growth and development across industries.
Read More
Durable Stainless Steel Industrial Pump for Your Business Needs
Stainless Steel Industrial Pump: A Reliable Solution for Industrial Pumping NeedsStainless steel industrial pumps are vital components for various industries such as oil and gas, chemical processing, food and beverage, and pharmaceuticals. These pumps are designed to handle corrosive and abrasive liquids, making them essential for the efficient operation of industrial processes. In this regard, {{Company Name}} is a leading manufacturer of high-quality stainless steel industrial pumps that are widely recognized for their durability, reliability, and performance.{{Company Name}} has been in the business of manufacturing industrial pumps for over three decades, and stainless steel pumps are one of its core product offerings. The company has invested heavily in research and development to engineer pumps that can withstand the harsh conditions of industrial applications. As a result, {{Company Name}}'s stainless steel industrial pumps are built to last, providing cost-effective and long-term solutions for its customers.One of the key features of {{Company Name}}'s stainless steel industrial pumps is their corrosion resistance. Stainless steel is known for its ability to resist corrosion, making it an ideal material for industrial pump construction. This property ensures that the pumps can handle aggressive and corrosive fluids without deteriorating over time, thus minimizing maintenance and replacement costs for the end-users.Moreover, {{Company Name}}'s stainless steel industrial pumps are designed for high performance. With their robust construction and precision engineering, these pumps are able to operate efficiently and reliably even in the most demanding industrial environments. This level of performance is crucial for maintaining the productivity and efficiency of industrial processes, ultimately leading to cost savings and operational excellence for the customers.In addition to their corrosion resistance and high performance, {{Company Name}}'s stainless steel industrial pumps are also known for their versatility. These pumps can be customized to meet the specific requirements of different industries and applications. Whether it's handling aggressive chemicals, high temperatures, or abrasive solids, {{Company Name}}'s stainless steel pumps can be tailored to deliver optimal performance in a wide range of industrial processes.Furthermore, {{Company Name}} is committed to providing comprehensive support and services for its stainless steel industrial pumps. The company has a team of experienced engineers and technical experts who work closely with customers to understand their pumping needs and provide customized solutions. From pump selection and installation to maintenance and troubleshooting, {{Company Name}}'s dedicated support ensures that customers get the most out of their stainless steel industrial pumps.With a strong focus on quality and customer satisfaction, {{Company Name}} has earned a reputation for being a trusted partner in the industrial pumping industry. The company's stainless steel industrial pumps are used by numerous well-known companies across different sectors, and they have consistently delivered superior performance and reliability.In conclusion, stainless steel industrial pumps are indispensable for the smooth operation of various industrial processes, and {{Company Name}} has established itself as a leading provider of high-quality stainless steel pumps. With their corrosion resistance, high performance, versatility, and comprehensive support, {{Company Name}}'s stainless steel industrial pumps offer a reliable solution for the pumping needs of industries worldwide. As the demand for efficient and durable pumping solutions continues to grow, {{Company Name}} remains at the forefront of delivering innovative and reliable stainless steel industrial pumps.
Read More
Sure! Please provide the original SEO title or the news content related to Horizontal Centrifugal so I can help rewrite it without the brand name.
Certainly! Please provide the company introduction text you'd like me to include, or any additional details you want featured in the news article about the horizontal centrifugal equipment.
Read More
Durable and Long Lasting Stainless Steel Pump Factory
Stainless Steel Pump Factory Leads the Way in Manufacturing ExcellenceStainless Steel Pump Factory, a leading manufacturer of stainless steel pumps, is revolutionizing the industry with its commitment to excellence, innovation, and quality. The company, which has been in operation for over 20 years, has established a reputation for producing high-performance pumps that are used in a variety of industries, including agriculture, pharmaceuticals, food and beverage, and water treatment.The factory, located in (location), is equipped with state-of-the-art machinery and technology, allowing for the production of pumps that meet the highest industry standards. With a focus on continuous improvement and research and development, Stainless Steel Pump Factory has been able to stay ahead of the competition and offer cutting-edge solutions to its customers.One of the key factors that sets Stainless Steel Pump Factory apart from its competitors is its unwavering commitment to quality. The company uses only the finest materials and components in the production of its pumps, ensuring that each product meets the highest standards of durability and performance. In addition, Stainless Steel Pump Factory has implemented rigorous quality control measures throughout the manufacturing process, guaranteeing that every pump that leaves the factory is of the highest quality.Another area in which Stainless Steel Pump Factory excels is innovation. The company's team of engineers and designers are constantly working on new and improved pump designs, incorporating the latest technological advancements to enhance performance and efficiency. This dedication to innovation has allowed Stainless Steel Pump Factory to stay at the forefront of the industry, continuously introducing new products that meet the evolving needs of its customers.In addition to its commitment to excellence and innovation, Stainless Steel Pump Factory is also dedicated to providing exceptional customer service. The company works closely with its clients to understand their specific needs and requirements, offering customized solutions to meet their individual applications. Furthermore, Stainless Steel Pump Factory provides comprehensive after-sales support, ensuring that customers can rely on their pumps for years to come.One of the most noteworthy aspects of Stainless Steel Pump Factory is its commitment to sustainability. The company recognizes the importance of minimizing its environmental impact and has implemented several initiatives to reduce energy consumption and waste generation. From using energy-efficient machinery to recycling materials, Stainless Steel Pump Factory is dedicated to operating in an environmentally responsible manner.Looking ahead, Stainless Steel Pump Factory is poised for continued success and growth in the industry. With a strong focus on quality, innovation, and customer service, the company is well-positioned to meet the evolving needs of its customers and maintain its leadership position in the market.As the demand for high-performance stainless steel pumps continues to grow across various industries, Stainless Steel Pump Factory is ready to meet the challenge and continue to deliver top-quality products. With its unwavering commitment to excellence, innovation, and customer satisfaction, Stainless Steel Pump Factory is truly a pioneer in the manufacturing of stainless steel pumps.
Read More
High-performance Multi Stage Fire Pumps for Maximum Efficiency
Multi Stage Fire Pump, a vital part of the fire protection system, has become a necessary tool for protecting lives and property. This innovative equipment is designed to act as a reliable and efficient water supply source in the event of a fire emergency. With its advanced technology and high performance, it has become an indispensable component in the firefighting industry.[Company Name] is proud to introduce its latest Multi Stage Fire Pump, which is engineered to meet the most stringent safety and performance standards. With a commitment to quality and innovation, [Company Name] has become a leading manufacturer of fire protection equipment, serving a diverse range of industries including commercial, industrial, and residential sectors. The Multi Stage Fire Pump is specifically designed to provide a continuous and reliable supply of water at high pressures, making it ideal for use in large buildings, manufacturing facilities, and other high-rise structures. Its multi-stage design allows for increased pressure and flow, ensuring that water can reach even the most challenging areas of a building during a fire emergency. This feature is critical in ensuring the safety and protection of occupants and assets within the building.In addition to its outstanding performance, the Multi Stage Fire Pump by [Company Name] is also known for its durability and reliability. Constructed with high-quality materials and precision engineering, this pump is built to withstand the harshest conditions and maintain optimal performance over the long term. The pump's robust design ensures that it can stand up to the rigors of firefighting operations, providing peace of mind to building owners and occupants.Furthermore, the Multi Stage Fire Pump is equipped with advanced monitoring and control systems, allowing for seamless integration into a building's fire protection infrastructure. Its user-friendly interface and remote monitoring capabilities make it easy to operate and maintain, ensuring that it can be effectively utilized in emergency situations. This level of sophistication and ease of use sets the Multi Stage Fire Pump apart from other options on the market, making it a preferred choice for architects, engineers, and building owners.[Company Name]'s commitment to excellence extends beyond just the product itself. The company is dedicated to providing comprehensive support and service to its customers, ensuring that they have access to the knowledge and expertise needed to make the most of their fire protection investments. This includes ongoing maintenance and inspection services, as well as access to a dedicated team of technical specialists who are available to assist with any questions or concerns.With its cutting-edge technology, superior performance, and exceptional customer support, the Multi Stage Fire Pump from [Company Name] is setting a new standard for fire protection in the industry. As buildings continue to grow in size and complexity, the need for advanced fire protection solutions becomes increasingly critical. The Multi Stage Fire Pump stands at the forefront of this evolution, providing the reliability and performance necessary to meet the demands of modern firefighting.In conclusion, the Multi Stage Fire Pump by [Company Name] represents a significant advancement in fire protection technology. Its innovative design, high performance, and comprehensive support make it the ideal choice for any building looking to enhance its fire protection capabilities. With [Company Name]'s commitment to excellence and customer satisfaction, the Multi Stage Fire Pump is poised to become a staple in fire protection systems for years to come.
Read More
Top Short Setting Pump Options on the Market Today
Short Setting Pump, a new innovative product in the field of industrial pumps, is set to revolutionize the way industrial pumping is done. This state-of-the-art pump is designed to provide efficient and reliable pumping solutions for a wide range of applications, making it an indispensable tool for industries across the globe.Short Setting Pump is a product of {} company, a renowned name in the field of industrial equipment and machinery. {} has been at the forefront of innovation, constantly striving to develop cutting-edge solutions to meet the evolving needs of industries. With its commitment to quality, reliability, and performance, {} has earned a reputation for excellence in the industry.The Short Setting Pump is the latest addition to {}'s extensive portfolio of industrial pumps, and it promises to deliver unmatched performance and efficiency. It is designed to handle a wide range of fluids, including corrosive, abrasive, and viscous liquids, making it suitable for diverse industrial applications. With its compact and lightweight design, the pump is easy to install and operate, making it a convenient choice for businesses looking for a reliable pumping solution.One of the key features of the Short Setting Pump is its adjustable settings, which allow users to customize the pump's operation according to their specific requirements. This flexibility makes the pump suitable for a variety of pumping tasks, from low-flow, high-pressure applications to high-flow, low-pressure operations. The pump's variable settings make it a versatile and cost-effective solution for industries looking to optimize their pumping processes.In addition to its advanced features, the Short Setting Pump is built to last, with a robust construction that ensures durability and longevity. The pump is designed to withstand the rigors of industrial use, making it a reliable and low-maintenance solution for businesses. Its high-performance motor and efficient design also contribute to its energy efficiency, helping businesses reduce their operational costs while maintaining high productivity.The introduction of the Short Setting Pump reflects {}'s ongoing commitment to innovation and customer satisfaction. {} understands the challenges faced by industries in managing their pumping needs, and the company's relentless pursuit of excellence has culminated in the development of this groundbreaking pump. With its exceptional performance, reliability, and versatility, the Short Setting Pump is poised to make a significant impact on the industrial pumping landscape.Customers can expect unparalleled support and service from {} when they choose the Short Setting Pump for their operations. {}'s team of experts is dedicated to helping businesses find the best pumping solutions for their specific needs, providing guidance and assistance every step of the way. Whether it's installation, maintenance, or troubleshooting, customers can rely on {} to deliver top-notch support and ensure the smooth operation of their pumps.With the introduction of the Short Setting Pump, {} is once again raising the bar for excellence in the industrial pumping industry. This innovative product is set to redefine the standards for performance, efficiency, and reliability, offering businesses a superior pumping solution that meets their diverse needs. As industries continue to evolve and grow, {} remains at the forefront, leading the way with cutting-edge technology and unparalleled expertise in industrial pumping solutions.
Read More
Ultimate Guide to Self-Priming Centrifugal Pumps: Everything You Need to Know
The company introduced their latest innovation, the Self Priming Centrifugal Pump, during a recent press conference. This new product is set to revolutionize the pumping industry with its advanced technology and efficiency.The Self Priming Centrifugal Pump is designed to be extremely versatile and easy to use. It can be used in a wide range of applications, including industrial, municipal, and agricultural settings. The pump is capable of handling a variety of fluids, including water, chemicals, and other liquids. This makes it an ideal choice for many different industries.One of the key features of the Self Priming Centrifugal Pump is its self-priming capability. This means that the pump is able to evacuate air from the suction line and prime itself without the need for external assistance. This makes it incredibly convenient and easy to use, saving time and effort for the operator.The pump is also designed to be highly efficient, with a streamlined design that minimizes energy consumption. This not only reduces operating costs, but also makes the pump more environmentally friendly. In addition, the pump is constructed from high-quality materials that ensure long-lasting performance and durability.During the press conference, the company's spokesperson highlighted the extensive research and development that went into the creation of the Self Priming Centrifugal Pump. The team of engineers and designers worked tirelessly to ensure that the pump meets the highest standards of quality and reliability. The result is a product that is truly state-of-the-art and represents the latest advancements in pumping technology.The spokesperson also emphasized the company's commitment to customer satisfaction. They stated that the Self Priming Centrifugal Pump is backed by a comprehensive warranty and after-sales support, ensuring that customers can have complete peace of mind when using the product.The company's CEO also spoke at the press conference, expressing their pride in the new product and the hard work of their team. They stated that the Self Priming Centrifugal Pump is a testament to the company's dedication to innovation and excellence. They also highlighted the pump's potential to make a positive impact in various industries, improving efficiency and reliability in fluid handling processes.Furthermore, the company announced that the Self Priming Centrifugal Pump will be available for purchase in the coming months, with distribution channels already being established. They are confident that the product will be well-received in the market, and they are looking forward to seeing the impact it will have on the pumping industry.In conclusion, the introduction of the Self Priming Centrifugal Pump represents a significant leap forward for the company's product line. With its cutting-edge technology, versatile capabilities, and focus on efficiency, the pump is sure to make a substantial impact in various industries. The company's dedication to quality and customer satisfaction is apparent in this latest innovation, and they are poised to set new standards with the Self Priming Centrifugal Pump.
Read More
Highly Efficient Centrifugal Pump for Industrial Use
Dn Ansi Centrifugal Pump Revolutionizes Pumping IndustryIn the ever-evolving world of industrial machinery, one company has taken the lead in designing innovative and efficient pumping solutions. With a focus on cutting-edge technology and a commitment to superior quality, {} has recently introduced the Dn Ansi Centrifugal Pump, a product that is set to revolutionize the pumping industry.The Dn Ansi Centrifugal Pump is designed to handle the most demanding industrial applications, offering high performance and reliability. These pumps are ideal for a wide range of industries including chemical, petrochemical, oil and gas, pharmaceutical, and water treatment. With a focus on durability and energy efficiency, these pumps are built to withstand the harshest operating conditions while minimizing energy consumption.One of the key features of the Dn Ansi Centrifugal Pump is its modular design, which allows for easy maintenance and servicing. This design also facilitates quick and hassle-free installation, reducing downtime and increasing overall operational efficiency. Additionally, the pumps are equipped with state-of-the-art monitoring and control systems, allowing for remote operation and real-time performance tracking.The company's commitment to innovation and excellence is evident in the development of the Dn Ansi Centrifugal Pump. With a team of experienced engineers and technicians, {} has employed the latest technologies and engineering principles to ensure that these pumps exceed industry standards. Rigorous testing and quality control measures are implemented throughout the production process, guaranteeing that each pump delivers consistent performance and reliability.{}'s dedication to customer satisfaction is reflected in the company's comprehensive after-sales support and technical assistance. Customers can rely on a network of service professionals who are trained to provide prompt and effective solutions to any operational issues. This commitment to customer service further sets {} apart from its competitors, solidifying the company's reputation as a leader in the pumping industry.With a proven track record of delivering innovative and reliable pumping solutions, {} has positioned itself as a trusted partner for companies seeking high-quality industrial equipment. The introduction of the Dn Ansi Centrifugal Pump further cements the company's standing as an industry leader, offering unmatched performance and efficiency in pumping technology.As industries continue to evolve and demand increases for more advanced and efficient pumping solutions, {} remains at the forefront, consistently raising the bar for excellence in industrial machinery. The Dn Ansi Centrifugal Pump is a testament to the company's unwavering commitment to innovation, quality, and customer satisfaction.In conclusion, the introduction of the Dn Ansi Centrifugal Pump by {} represents a significant milestone in the pumping industry. With its cutting-edge design, superior performance, and unmatched reliability, these pumps are set to revolutionize industrial pumping applications. {}'s dedication to excellence and customer satisfaction ensures that the company will continue to lead the way in providing innovative and efficient pumping solutions for years to come.
Read More
Durable and Efficient Belt Gear Pump for Industrial Applications
Belt Gear Pump Revolutionizes Pumping Technology: The Future of Efficient Fluid TransferIn today's fast-paced industrial landscape, the demand for efficient and reliable fluid transfer solutions has never been greater. With the introduction of the innovative Belt Gear Pump, manufacturers and operators can expect a paradigm shift in their pumping operations. This cutting-edge technology, developed by {}, is set to revolutionize the way fluids are transferred in a wide range of industrial applications.The Belt Gear Pump is a state-of-the-art solution that combines advanced engineering principles with practical design features. It is the result of years of research and development, with a focus on creating a pump that is not only highly efficient but also durable and easy to maintain. The pump's unique design allows for smooth and continuous fluid transfer, making it ideal for processes that require a consistent flow of liquids.One of the key features of the Belt Gear Pump is its high level of efficiency. Unlike traditional pumps, which may be prone to energy wastage and inefficiencies, the Belt Gear Pump is designed to maximize the transfer of fluids while minimizing energy consumption. This not only helps to reduce operational costs but also makes it an environmentally friendly choice for industrial applications.The reliability of the Belt Gear Pump is another standout feature that sets it apart from other pumping solutions. With a robust construction and high-quality materials, this pump is built to withstand the rigors of industrial use. Its durability ensures that operators can rely on it to perform consistently, even in demanding operating conditions. Additionally, the pump's design minimizes the risk of downtime and maintenance, contributing to overall operational efficiency.In terms of maintenance, the Belt Gear Pump is designed with user-friendliness in mind. Its modular construction allows for easy access to components, making maintenance and servicing simple and straightforward. This not only reduces downtime for maintenance but also minimizes the need for specialized skills or tools, making it a cost-effective choice for operators.Another highlight of the Belt Gear Pump is its versatility. It is designed to handle a wide range of fluids, including viscous liquids, abrasive slurries, and corrosive chemicals. This makes it suitable for diverse industrial applications, from chemical processing and mining to food and beverage production. Its ability to handle different types of fluids makes it a versatile and adaptable choice for a variety of industries.{} is known for its commitment to innovation and customer satisfaction. The company has a strong track record of developing cutting-edge pumping solutions that deliver exceptional performance and reliability. With the Belt Gear Pump, the company has once again raised the bar for pumping technology, showcasing its dedication to advancing the industry and meeting the needs of its customers.As the industrial landscape continues to evolve, the demand for efficient fluid transfer solutions will only grow. The Belt Gear Pump is poised to meet this demand head-on, offering a game-changing solution for operators and manufacturers seeking to optimize their pumping operations. With its focus on efficiency, reliability, and versatility, this innovative pump represents the future of fluid transfer technology.In conclusion, the Belt Gear Pump, developed by {}, is a game-changing solution for a wide range of industrial pumping applications. With its focus on efficiency, reliability, and versatility, this innovative pump is set to revolutionize the way fluids are transferred in the industrial landscape. As the industry continues to evolve, the Belt Gear Pump stands out as a cutting-edge solution that sets a new standard for fluid transfer technology.
Read More