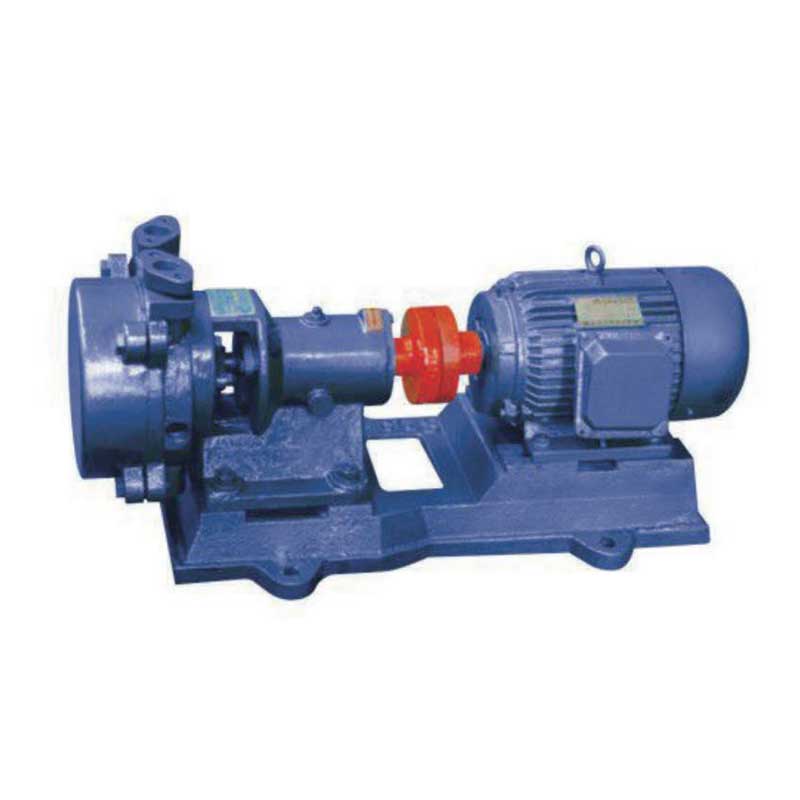
Submerged Pumps for Acidic Environments - What You Need to Know
Acid Submersible Pumps Used in () Industries Showcased by ()In the realm of industrial manufacturing and processing, the need for durable and efficient equipment is paramount. One of the crucial components in various industrial processes is the acid submersible pump, which serves the purpose of transferring corrosive liquids with high efficiency and reliability. Among the leading manufacturers of such industrial pumps is (), a renowned company known for its cutting-edge technology and top-quality products.() has recently showcased their acid submersible pumps at a prominent industrial equipment exhibition, drawing the attention of industry professionals and potential clients alike. With a steadfast commitment to innovation and excellence, () has become a trusted name in the realm of industrial pumps, offering a wide range of pumping solutions tailored to the specific needs of various industries.The acid submersible pumps offered by () are designed to handle the challenges posed by corrosive and abrasive liquids, making them an ideal choice for industries dealing with chemical processing, mining, wastewater treatment, and other similar applications. These pumps are manufactured using high-grade materials that are resistant to corrosion, ensuring long-term reliability and performance.One of the key features of ()'s acid submersible pumps is their advanced design, which incorporates efficient impellers and motor systems that are capable of handling the demands of transferring corrosive fluids. In addition, these pumps are equipped with robust sealing mechanisms to prevent leaks and ensure safe operation, even in the harshest industrial environments.Moreover, () offers a range of customization options for their acid submersible pumps, allowing clients to select the most suitable pump configuration based on their specific requirements. Whether it's the capacity, head, or materials of construction, () provides a comprehensive solution to meet the diverse needs of its industrial clients.In line with their commitment to customer satisfaction, () also provides reliable after-sales support and maintenance services for their pumps, ensuring that clients can maximize the longevity and performance of their equipment. This comprehensive approach has earned () a distinguished reputation in the industry, with a long list of satisfied clients who attest to the quality and reliability of their products."We take pride in delivering pumping solutions that surpass the expectations of our clients, especially when it comes to handling corrosive liquids," said a spokesperson for (). "Our acid submersible pumps are the result of extensive research and development, combined with our deep understanding of the challenges faced by industries dealing with corrosive fluids. We are dedicated to providing our clients with the most reliable and efficient pumping solutions, tailored to their specific needs."With a strong focus on technological innovation and product development, () continues to set new benchmarks in the realm of industrial pumps, including their acid submersible pumps. The company's commitment to excellence and customer satisfaction has positioned them as a preferred choice for industries requiring reliable pumping solutions for their corrosive fluid handling needs.As the industrial landscape continues to evolve, the demand for efficient and durable pumping equipment will only intensify. Companies like () are at the forefront of meeting this demand, offering advanced pumping solutions that empower industries to achieve their production goals with utmost reliability and efficiency.In conclusion, the showcase of ()'s acid submersible pumps at the recent industrial equipment exhibition is a testament to the company's dedication to innovation and excellence. As industries continue to seek reliable pumping solutions for handling corrosive fluids, () is well-positioned to meet this demand with their top-quality and efficient acid submersible pumps. With a focus on customer satisfaction and technological innovation, () is set to further solidify its position as a leading provider of industrial pumping solutions.
Read More
Vertical Multistage Pipeline Pump: Features, Benefits, and Applications
Certainly! Please provide the specific news content about the Vertical Multistage Pipeline Pump and the company introduction you would like me to incorporate.
Read More
Single Stage Single Suction Chemical Pump for Efficient Fluid Handling
Certainly! Please provide the specific news content about the Single Stage Single Suction Chemical Pump and the company introduction you would like me to use. Once I have those details, I can draft an 800-word news article for you.
Read More
Top Double Suction Pump: Key Features and Benefits You Should Know About
[Company Name] Unveils Revolutionary Double Suction Pump[Company Name], a leader in industrial fluid handling solutions, has recently unveiled its latest innovation – the Double Suction Pump. This ground-breaking product is set to redefine the industry with its superior performance and innovative design.The Double Suction Pump is designed to handle large volumes of liquid with high efficiency and minimal vibration. Its unique double-suction impeller design allows for a balanced axial thrust, resulting in smoother operation and extended equipment life. With a robust construction and advanced hydraulic design, this pump is capable of delivering high flow rates and excellent head coverage, making it the ideal choice for a wide range of industrial applications.“We are excited to introduce the Double Suction Pump to the market,” said [Company Name]’s CEO. “This product represents a significant advancement in fluid handling technology, and we are confident that it will set a new standard for performance and reliability in the industry.”In addition to its exceptional performance, the Double Suction Pump is also designed with ease of maintenance in mind. Its modular construction allows for quick and convenient access to internal components, making routine maintenance and repairs a simple task. This not only minimizes downtime but also reduces overall operating costs for the end user.Furthermore, the Double Suction Pump is equipped with state-of-the-art monitoring and control systems, allowing for seamless integration into existing industrial processes. This enables users to optimize their operations and achieve higher levels of efficiency and productivity.[Company Name] has a long-standing reputation for delivering high-quality and reliable fluid handling solutions. With a global presence and a strong commitment to customer satisfaction, the company has built a loyal customer base and has established itself as a trusted partner for industrial organizations around the world.The introduction of the Double Suction Pump further solidifies [Company Name]’s position as an industry leader. This latest innovation is a testament to the company’s dedication to continuous improvement and its ability to anticipate and meet the evolving needs of its customers.The Double Suction Pump is available in a range of sizes and configurations to accommodate diverse application requirements. Whether it’s for water supply and distribution, HVAC systems, or industrial processes, this pump is designed to deliver unmatched performance and reliability.With its cutting-edge design, exceptional performance, and user-friendly features, the Double Suction Pump is poised to become the go-to solution for industrial fluid handling needs. Whether it's for new installations or as a replacement for existing equipment, this product is set to make a significant impact on the industry.As [Company Name] continues to push the boundaries of innovation and excellence, the Double Suction Pump is a clear example of its commitment to delivering value and performance to its customers. With its launch, the company has once again raised the bar for the industry, setting new standards for efficiency, reliability, and overall performance in fluid handling solutions.In conclusion, the unveiling of the Double Suction Pump marks another milestone for [Company Name] and reinforces its position as a pioneering force in the industry. This latest innovation is a testament to the company's unwavering commitment to delivering cutting-edge solutions that meet and exceed the needs of its customers. With its superior performance, innovative design, and user-friendly features, the Double Suction Pump is set to revolutionize industrial fluid handling and set new benchmarks for excellence.
Read More
High-Quality Belt Gear Pumps for Efficient Fluid Transfer
Certainly! Please provide the specific news content about the Belt Gear Pump and the company introduction {} so I can craft the 800-word news article for you.
Read More
High-Quality Stainless Steel Centrifugal Magnetic Pump for Industrial Use
This just in: a groundbreaking development in the world of industrial pumps has been announced by {company name}. The company, known for its innovative and cutting-edge technologies, has revealed the latest addition to its impressive lineup of industrial equipment: the Stainless Steel Centrifugal Magnetic Pump. This new pump is set to revolutionize the industry with its advanced features and capabilities, offering an unparalleled level of performance and efficiency.The Stainless Steel Centrifugal Magnetic Pump is the result of years of research and development by {company name}. Leveraging the expertise of its team of engineers and scientists, the company has engineered a pump that sets new standards for reliability, durability, and performance. With its state-of-the-art design and construction, this pump is poised to deliver exceptional results in a wide range of industrial applications.One of the key highlights of the Stainless Steel Centrifugal Magnetic Pump is its use of advanced magnetic technology. Unlike traditional pumps that rely on mechanical seals to prevent leakage and contamination, this pump utilizes a magnetic drive system to ensure a completely leak-free operation. This not only enhances the safety and reliability of the pump but also eliminates the need for regular maintenance and replacement of seals, reducing downtime and operating costs for businesses.Furthermore, the pump's stainless steel construction offers superior corrosion resistance, making it suitable for handling a variety of aggressive and corrosive fluids. Whether it's chemicals, solvents, acids, or alkalis, this pump is designed to withstand the harshest operating conditions, providing businesses with a versatile and robust solution for their fluid handling needs.In addition to its advanced materials and construction, the Stainless Steel Centrifugal Magnetic Pump boasts a high-efficiency impeller and motor design, ensuring optimal performance and energy savings. With its smooth and quiet operation, this pump is designed to minimize vibration and noise, creating a more conducive work environment for operators."We are thrilled to introduce the Stainless Steel Centrifugal Magnetic Pump to the market," said {spokesperson's name}, {title} at {company name}. "This pump represents a significant advancement in industrial pumping technology and embodies our commitment to delivering innovative solutions that meet the evolving needs of our customers. We believe that the unique combination of advanced features and high performance will set a new standard for industrial pumps and provide our customers with a competitive edge in their operations."The launch of the Stainless Steel Centrifugal Magnetic Pump underscores {company name}'s position as a leader in the industrial equipment industry. With a track record of delivering high-quality products and a dedication to innovation, the company has earned the trust and confidence of customers worldwide. By continually pushing the boundaries of what is possible in industrial technology, {company name} remains at the forefront of the industry, shaping the future of industrial operations.As businesses across various sectors continue to seek reliable and efficient solutions for fluid handling and transfer, the Stainless Steel Centrifugal Magnetic Pump is poised to meet these demands head-on. With its cutting-edge technology, exceptional performance, and robust construction, this pump is set to make a lasting impact in industries such as chemical processing, pharmaceuticals, food and beverage, and many others.For more information about the Stainless Steel Centrifugal Magnetic Pump and other innovative products from {company name}, visit their website at {company website}. With a commitment to excellence and a passion for innovation, {company name} remains a trusted partner for businesses seeking the best in industrial equipment and technologies.
Read More
How to Choose the Best Pump for Your Needs: A Comprehensive Guide
Cpump, a leading provider of innovative solutions in the field of fluid pumping systems, has recently announced the launch of their latest product designed to revolutionize the way companies handle fluid pumping processes. With a strong focus on efficiency, reliability, and sustainability, Cpump has firmly established itself as a trailblazer in the industry, and their newest offering is poised to further solidify their position as a market leader.The newest product from Cpump is a state-of-the-art fluid pumping system that is designed to meet the diverse needs of modern industries. Whether it is for transporting water, chemicals, or other fluids, this system offers unparalleled performance and versatility. The system is equipped with cutting-edge technology that allows for precise control and monitoring, ensuring optimal efficiency and minimal wastage. This level of precision is especially crucial in industries where accuracy is of utmost importance, such as pharmaceuticals, food and beverage, and chemical production.One of the key highlights of Cpump's new product is its sustainability features. The system is engineered to minimize energy consumption, thereby reducing the carbon footprint of the operations it is involved in. This aligns with Cpump's commitment to environmental responsibility and their dedication to developing solutions that support a greener future. The system is also built to last, with a robust design that ensures durability and longevity, further contributing to sustainability by minimizing the need for frequent replacements and repairs.In addition to its impressive performance and sustainability benefits, Cpump's new fluid pumping system also offers a high level of reliability. This is crucial for industries where downtime can result in significant losses. The system is designed to operate smoothly and consistently, with minimal risk of malfunctions or breakdowns. This reliability is further enhanced by Cpump's exceptional customer support and maintenance services, ensuring that their clients can always count on uninterrupted operation.Cpump has a long-standing reputation for delivering cutting-edge solutions that are tailored to meet the specific needs of their clients. The company takes a collaborative approach, working closely with their customers to understand their requirements and develop customized solutions that address their unique challenges. This customer-centric philosophy has earned Cpump the trust and loyalty of a diverse range of industries, including but not limited to, oil and gas, mining, water and wastewater, and power generation.With the launch of their latest product, Cpump is poised to set new benchmarks in the fluid pumping industry. The system's advanced features, coupled with Cpump's renowned expertise and commitment to excellence, make it a game-changer that is set to reshape the way companies handle fluid pumping processes. As industries continue to evolve and strive for greater efficiency and sustainability, Cpump remains at the forefront, consistently raising the bar and setting new standards for what is possible in fluid pumping technology.For companies seeking a reliable, efficient, and sustainable solution for their fluid pumping needs, Cpump's new system offers a compelling proposition. With its cutting-edge technology, dedication to sustainability, and unwavering commitment to customer satisfaction, Cpump has once again demonstrated why they are a leading force in the fluid pumping industry. As industries continue to grapple with the challenges of an ever-changing landscape, Cpump stands ready to provide the solutions needed to thrive and succeed in the 21st century.
Read More
Top Chemical Process Pumps for Industrial Applications
Chemical Process Pump, a leading manufacturer of industrial pumps, is proud to announce the release of their latest innovative pump technology. The company has been at the forefront of the pumping industry for over 50 years, consistently delivering high-quality, reliable pumps to a wide range of industrial sectors.The new chemical process pump is the result of years of research and development, and represents a significant advancement in pump technology. Designed to meet the demanding requirements of chemical processing facilities, the pump offers unmatched performance, efficiency, and durability.One of the key features of the new pump is its advanced sealing technology, which ensures a leak-free operation even when handling the most corrosive and abrasive chemicals. This is crucial for ensuring the safety and reliability of chemical processing operations, as any leaks or spills could have disastrous consequences.In addition, the pump is constructed from high-grade materials that are resistant to corrosion, erosion, and abrasion, ensuring a long service life even in the most challenging operating conditions. This reliability is further enhanced by the pump's rugged design and robust construction, which are built to withstand the rigors of industrial environments.The new pump also offers a high level of efficiency, helping chemical processing facilities to reduce their energy consumption and operating costs. This is achieved through the use of advanced hydraulic design and precision engineering, which minimize friction and maximize the pump's performance.Furthermore, the pump is designed for easy maintenance, with quick and simple access to key components for inspection and servicing. This reduces downtime and ensures that the pump can be kept in optimal working condition with minimal effort.Chemical Process Pump is dedicated to providing its customers with the highest level of support and service, and the release of this new pump is a testament to their ongoing commitment to innovation and excellence. The company's team of engineers and technical experts have worked tirelessly to develop this cutting-edge technology, and are confident that it will make a significant impact in the chemical processing industry.The new pump is available in a range of sizes and configurations to suit the specific needs of different chemical processing applications. Whether it's handling aggressive chemicals, high temperatures, or demanding operating conditions, the pump is capable of delivering the performance and reliability required.Chemical Process Pump has a long-standing reputation for delivering exceptional pumping solutions to industries such as chemical processing, petrochemical, pharmaceutical, and many others. The company's pumps are known for their durability, reliability, and performance, and are trusted by some of the largest industrial facilities around the world.With the release of this new pump, Chemical Process Pump has once again demonstrated their ongoing commitment to pushing the boundaries of pump technology and delivering innovative solutions to their customers. The company is confident that this new pump will set new standards for performance and reliability in the chemical processing industry, and looks forward to seeing the positive impact it will have on its customers' operations.In conclusion, the release of the new chemical process pump represents a significant milestone for Chemical Process Pump and reaffirms the company's position as a leader in the industrial pumping industry. With its advanced technology, reliability, and efficiency, the pump is set to become the go-to solution for chemical processing facilities looking to optimize their operations and enhance their safety and productivity.
Read More
Highly Efficient End Suction Back Pull Out Centrifugal Pump for Industrial Use
In a world where industrial efficiency is paramount, the demand for high-quality pumping solutions has never been greater. With this in mind, it is with great excitement that we announce the release of a new End Suction Back Pull Out Centrifugal Pump from (company name). This cutting-edge pump represents the culmination of years of research, development, and innovation, and it promises to deliver unparalleled performance across a wide range of industrial applications.The End Suction Back Pull Out Centrifugal Pump is designed to meet the needs of modern industrial processes, providing a reliable and efficient solution for a variety of pumping challenges. Its innovative design and state-of-the-art technology ensure that it delivers high performance, low maintenance, and maximum energy efficiency, making it an ideal choice for a wide range of industries.One of the key features of the End Suction Back Pull Out Centrifugal Pump is its robust construction. The pump is built to withstand the rigors of industrial use, with high-quality materials and precision engineering ensuring long-lasting reliability and performance. This means that it can be relied upon to deliver consistent results, even in the most demanding of environments.Furthermore, the pump's versatile design allows it to be easily adapted to suit specific requirements, making it a highly flexible solution for a wide range of applications. Whether it's used for water supply, heating and air conditioning, pressure boosting, or industrial processes, this pump can be tailored to meet the unique needs of any industry.What sets the End Suction Back Pull Out Centrifugal Pump apart from its competitors is its efficiency. Thanks to its advanced hydraulics and innovative design, the pump is able to deliver impressive flow rates and high head levels while minimizing energy consumption. This not only reduces operating costs but also minimizes the environmental impact of industrial processes, making it a sustainable choice for businesses looking to improve their green credentials.In addition to its impressive performance, the pump is also designed with ease of maintenance in mind. Its back pull-out design allows for quick and convenient access to the pump's internal components, facilitating straightforward servicing and minimizing downtime. This ensures that any maintenance tasks can be carried out efficiently, keeping the pump operating at peak performance levels at all times.The release of the End Suction Back Pull Out Centrifugal Pump represents a significant milestone for (company name), highlighting our ongoing commitment to providing the highest quality pumping solutions to our customers. With our extensive experience in the industry and a dedication to innovation, we have developed a pump that not only meets the needs of modern industrial processes but also sets new standards for performance, reliability, and efficiency.As a company, we pride ourselves on our ability to deliver cutting-edge pumping solutions that empower our customers to achieve their goals. With the release of the End Suction Back Pull Out Centrifugal Pump, we are confident that we are providing a solution that will help businesses to improve their operations, reduce their environmental impact, and enhance their overall efficiency.In conclusion, the End Suction Back Pull Out Centrifugal Pump from (company name) represents a significant advancement in pumping technology. With its high performance, efficiency, and reliability, it is poised to become the go-to choice for businesses across a wide range of industries. As we continue to push the boundaries of what is possible in the world of pumping solutions, we are excited to see the positive impact that this pump will have on the industrial landscape.
Read More
High-Performance Horizontal Multi Stage Fire Pump for Efficient Fire Protection
Horizontal Multi-Stage Fire Pump: A Crucial Safety Solution for Commercial and Industrial BuildingsIn any commercial or industrial building, fire safety is of paramount importance. When a fire breaks out, the ability to quickly and effectively extinguish it can mean the difference between minor damage and devastating loss. That's why having a reliable and efficient fire pump system in place is essential for ensuring the safety of occupants and protecting valuable assets.Today, we're proud to introduce our high-quality horizontal multi-stage fire pump, which is designed to meet the rigorous demands of modern fire protection systems. Our pump, which is manufactured with precision engineering and cutting-edge technology, offers superior performance and reliability in the event of a fire emergency.Key Features and BenefitsOur horizontal multi-stage fire pump is built to the highest standards, incorporating a range of advanced features that make it an ideal choice for a wide variety of commercial and industrial applications. Some of the key features and benefits of our fire pump include:1. High Efficiency: Our fire pump is designed for maximum efficiency, ensuring that water is delivered at the required pressure and flow rate to suppress fires effectively.2. Robust Construction: The pump is constructed from high-quality materials and components, making it durable and resistant to wear and tear, even in demanding environments.3. Easy Maintenance: With a modular design and easy access to key components, our fire pump is simple to maintain, saving time and reducing downtime.4. Compact Footprint: The horizontal configuration of the pump allows it to be easily integrated into existing fire protection systems, even in spaces with limited room.5. Compliance with Standards: Our fire pump meets all relevant industry standards and regulations, providing peace of mind that it will perform reliably when needed.ApplicationsOur horizontal multi-stage fire pump is suitable for a wide range of applications, including:- Office Buildings- Shopping Malls- Industrial Facilities- Warehouses- Hospitals- Data Centers- HotelsCompany Introduction{Company Name} is a leading manufacturer of fire protection equipment and systems, with a strong commitment to innovation, quality, and customer satisfaction. With over {number} years of experience in the industry, we have earned a reputation for excellence and reliability, serving clients across {location} and beyond.At {Company Name}, we understand the critical importance of fire safety, and we are dedicated to providing the highest quality products and solutions to help our customers safeguard their properties and personnel. Our horizontal multi-stage fire pump is the latest addition to our extensive product lineup, and we are proud to offer this state-of-the-art solution to our clients.In addition to our fire pump, we also provide a comprehensive range of fire protection systems, including fire suppression systems, fire alarms, and firefighting equipment. We offer design, installation, and maintenance services, ensuring that our clients have access to everything they need to create a safe and secure environment.Our team of skilled engineers and technicians is committed to delivering exceptional service and support, working closely with our clients to understand their unique requirements and provide tailored solutions that meet their needs.ConclusionWith the introduction of our horizontal multi-stage fire pump, {Company Name} continues to demonstrate our dedication to innovation and excellence in fire protection. We are confident that our pump will serve as a valuable asset for commercial and industrial buildings, providing the reliability and performance needed to ensure effective fire suppression.As we look to the future, we are committed to further expanding our product range and continuing to raise the bar for fire safety solutions. With {Company Name} as your partner, you can have confidence that your fire protection needs are in good hands.
Read More