
Sure! Please provide the news content or the title you want me to rewrite.
By:Admin
Company News & Blog
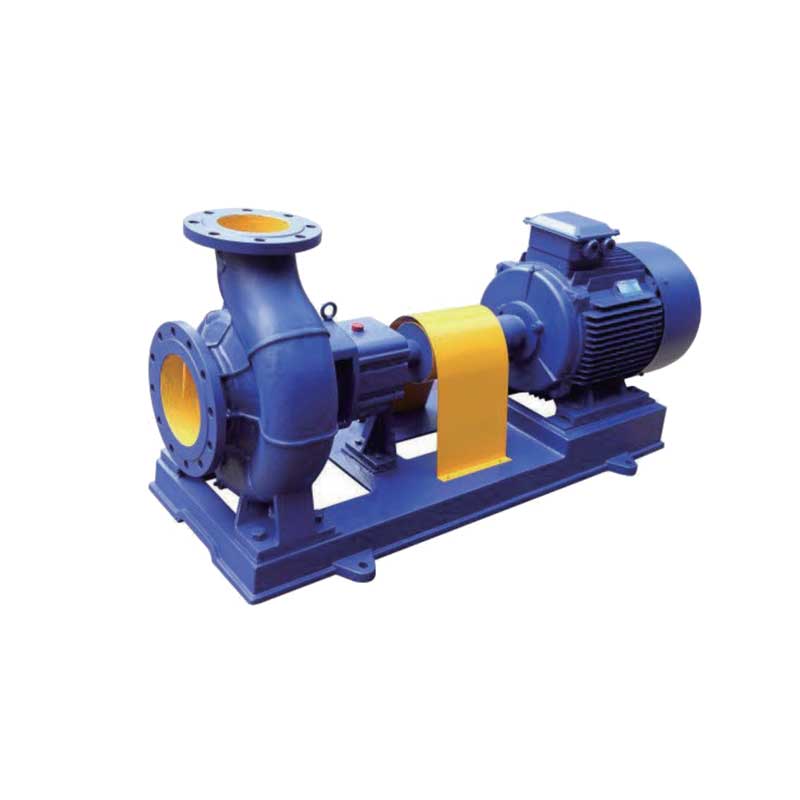
High-quality Slurry Pump for Efficient Material Handling
Slurry Pump Company, a leading provider of innovative slurry pump solutions, has been making waves in the industry with its cutting-edge technologies and commitment to customer satisfaction. With a strong focus on research and development, the company has been at the forefront of developing efficient and reliable slurry pump systems that meet the ever-evolving needs of the mining, oil and gas, and industrial sectors.The company, headquartered in [location], has a state-of-the-art manufacturing facility that is equipped with the latest machinery and technologies to produce high-quality slurry pumps that can withstand the most demanding applications. Its team of experienced engineers and technicians work tirelessly to ensure that every pump that leaves the facility meets the highest standards of performance and durability.One of the company's flagship products is its [product name] slurry pump, which has gained a reputation for its exceptional performance and reliability in handling abrasive and corrosive slurries. The [product name] pump is designed to deliver high efficiency and low maintenance, making it a preferred choice for a wide range of industries. Its unique design features and materials make it suitable for pumping heavy-duty slurries with minimal wear and tear, leading to cost savings and increased productivity for its users.In addition to its [product name] pump, the company also offers a comprehensive range of slurry pumps, including submersible pumps, vertical pumps, and horizontal pumps, to cater to various application requirements. Each pump is designed and manufactured with precision to ensure seamless operation and maximum performance in challenging environments.The company's commitment to quality and innovation is further exemplified by its continuous investment in research and development. It consistently seeks to improve its products and develop new technologies to stay ahead of the competition and provide its customers with the best solutions for their pumping needs.Moreover, the company has a dedicated team of customer service professionals who work closely with clients to understand their specific requirements and provide tailored solutions. From initial consultation to after-sales support, the company ensures that its customers receive the highest level of service and assistance throughout their journey with its products.Furthermore, the company has a strong global presence, with a network of distributors and partners in key regions around the world. This enables it to reach a wide customer base and provide prompt and reliable support to its clients, regardless of their location.A spokesperson for Slurry Pump Company commented, "We are proud to be a leader in the slurry pump industry, and we are dedicated to continuing our tradition of excellence and innovation. Our goal is to provide our customers with the most reliable and efficient pumping solutions that enable them to enhance their operations and achieve their business objectives."With its unwavering commitment to excellence, a track record of delivering top-quality products, and a customer-centric approach, Slurry Pump Company is poised to continue its success in the industry and solidify its position as a trusted partner for slurry pump solutions. Whether in the mining, oil and gas, or industrial sectors, the company's innovative pumping technologies are sure to make a lasting impact and drive efficiency for its customers.
High-Quality Chemical Transfer Pumps for Efficient Fluid Handling
Certainly! Please provide the specific news content regarding the Chemical Transfer Pump and the company introduction you’d like me to use. Once I have those details, I’ll draft an 800-word news article for you.
High-Quality Multistage Pump Factory Offers Reliable Solutions
Dg Multistage Pump Factory, a leading manufacturer of industrial pumps, has been making waves in the industry with its innovative and high-quality products. With a strong focus on research and development, the company has cemented its position as a reliable and trusted supplier of multistage pumps for various applications.Established in [], Dg Multistage Pump Factory has grown from strength to strength, constantly evolving and adapting to meet the changing needs of its customers. The company has invested heavily in state-of-the-art manufacturing facilities, ensuring that its pumps are manufactured to the highest standards of quality and precision.Dg Multistage Pump Factory offers a wide range of multistage pumps, including [] series, [] series, and [] series. These pumps are designed to deliver exceptional performance, reliability, and efficiency, making them ideal for use in various industries such as [].One of the key factors that set Dg Multistage Pump Factory apart from its competitors is its commitment to innovation. The company has a dedicated team of engineers and researchers who are constantly working on developing new and improved pump technologies. This relentless pursuit of innovation has allowed Dg Multistage Pump Factory to stay ahead of the curve and provide its customers with cutting-edge pump solutions.In addition to its focus on innovation, Dg Multistage Pump Factory also places a strong emphasis on customer satisfaction. The company works closely with its clients to understand their specific needs and requirements, and then provides customized pump solutions to meet those needs. This customer-centric approach has earned Dg Multistage Pump Factory a reputation for being a responsive and reliable partner.Furthermore, Dg Multistage Pump Factory is committed to upholding the highest standards of quality and reliability in all its products. The company works in compliance with [] standards and holds various certifications that attest to the quality of its pumps. This commitment to quality has earned Dg Multistage Pump Factory the trust and loyalty of its customers.Moreover, Dg Multistage Pump Factory places a strong emphasis on sustainability and environmental responsibility. The company is constantly exploring ways to make its manufacturing processes more environmentally friendly and is committed to reducing its environmental impact. This commitment to sustainability aligns with the company's values and resonates with customers who are increasingly mindful of the environmental impact of the products they use.Looking ahead, Dg Multistage Pump Factory is poised for continued success and growth. The company has ambitious plans to expand its product range, enter new markets, and further strengthen its position as a leader in the industry. With its unwavering commitment to innovation, quality, and customer satisfaction, Dg Multistage Pump Factory is well-equipped to meet the evolving needs of its customers and remain a trusted partner for all their pump requirements.
Top-Quality Multistage Feed Pump for High Efficiency
High Quality Multistage Feed Pump Revolutionizing the IndustryThe [Company Name] has launched an innovative and high-quality LG series multistage feed pump that is set to revolutionize the industry. The company, renowned for its cutting-edge technology, has introduced this advanced pump to meet the growing demand for efficient and reliable pumping solutions in various industries.The LG series multistage feed pump is designed to deliver superior performance and reliability, making it the ideal choice for a wide range of applications. It is engineered to handle high-pressure pumping requirements with ease, making it suitable for use in industrial processes, water treatment plants, power generation facilities, and more.One of the key features of the LG series multistage feed pump is its durable and corrosion-resistant construction. The pump is built to withstand the harshest operating conditions, ensuring long-term reliability and minimal maintenance requirements. This makes it a cost-effective solution for businesses looking to reduce operational downtime and maintenance costs.In addition to its robust construction, the LG series multistage feed pump is also equipped with advanced technology that enhances its performance and efficiency. The pump features precision-engineered components that work seamlessly together to deliver a consistent and reliable flow of liquid, making it the preferred choice for critical pumping applications.Furthermore, the LG series multistage feed pump is designed for easy installation and maintenance, providing businesses with a hassle-free pumping solution that minimizes downtime and maximizes productivity. Its user-friendly design and intuitive controls make it easy to operate, while its modular construction allows for quick and simple maintenance procedures.The introduction of the LG series multistage feed pump is a testament to [Company Name]'s commitment to innovation and excellence. The company, which has a proven track record of delivering high-quality pumping solutions, has once again raised the bar with this latest addition to its product line.[Company Name] has consistently been at the forefront of technological advancements in the pumping industry, and the LG series multistage feed pump is a testament to its dedication to meeting the evolving needs of its customers. By combining cutting-edge technology with the highest quality materials and engineering expertise, the company has developed a pump that sets new standards for performance, reliability, and efficiency.The LG series multistage feed pump is the result of extensive research and development, as well as a deep understanding of the unique challenges and requirements of various industries. It is a reflection of [Company Name]'s unwavering commitment to providing its customers with the most advanced and reliable pumping solutions available on the market.With the launch of the LG series multistage feed pump, [Company Name] has once again demonstrated its leadership in the pumping industry. The company's dedication to innovation, quality, and customer satisfaction sets it apart from its competitors, making it the preferred choice for businesses seeking reliable and efficient pumping solutions.In conclusion, the introduction of the LG series multistage feed pump marks a significant milestone for [Company Name] and the pumping industry as a whole. With its exceptional performance, reliability, and efficiency, this innovative pump is set to revolutionize pumping solutions across various industries. As [Company Name] continues to push the boundaries of technological advancements, it remains the go-to choice for businesses looking for high-quality and cutting-edge pumping solutions.
High-Quality Centrifugal Pump for Efficient Fluid Handling
Certainly! Please provide the specific news content about the centrifugal pump and the company introduction you would like me to use. Once I have those, I can draft an 800-word news article for you without the brand name.
Highly Efficient Canned Motor Pump - A Game Changer in Pump Technology
Canned Motor Pump: The Future of Pump TechnologyIn the world of industrial and commercial pumping, efficiency, reliability, and safety are paramount. A company has emerged as a leader in addressing these concerns with their innovative Canned Motor Pump technology. With a long history of providing high-quality pumping solutions for a wide range of industries, they have solidified their reputation as a trusted and reliable partner for companies looking to optimize their pumping processes.The Canned Motor Pump is a unique and revolutionary design that offers several key advantages over traditional pump technologies. One of the most significant benefits is its hermetically sealed design, which eliminates the risk of leakage and environmental contamination. This is particularly important for industries such as chemical processing, where the safe handling of corrosive or hazardous materials is of utmost importance.The Canned Motor Pump also offers unparalleled energy efficiency, with its integrated motor design eliminating the need for complex and maintenance-intensive coupling systems. This not only reduces the overall footprint of the pump but also results in substantial energy savings over the lifetime of the equipment. In an era where environmental sustainability and cost-effectiveness are key considerations for businesses, this level of efficiency is a game-changer.Furthermore, the Canned Motor Pump's compact and modular design makes it easy to install and maintain, offering greater flexibility and convenience for operators. With fewer moving parts and a simplified construction, the pump requires minimal maintenance and has a longer operational lifespan than traditional pump systems, minimizing downtime and decreasing overall lifecycle costs.The company behind this groundbreaking technology has a proven track record of delivering high-quality pumping solutions to a diverse range of industries. With a strong focus on research and development, they are constantly pushing the boundaries of pump technology to meet the evolving needs of their customers. Their team of experienced engineers and technicians work closely with clients to develop customized pumping solutions that deliver maximum performance and reliability for any application.In addition to their cutting-edge technology, the company is committed to providing exceptional customer support and service. From initial consultation and system design to installation, training, and ongoing maintenance, they offer end-to-end support to ensure that their customers get the most out of their pumping systems. This level of dedication and expertise has earned them a reputation as a trusted partner for companies worldwide.As industries continue to evolve and face new challenges, the need for innovative and efficient pumping solutions has never been greater. The Canned Motor Pump technology offered by this company represents a significant leap forward in pump design, offering superior performance, energy efficiency, and reliability. With a strong focus on customer satisfaction and a commitment to pushing the boundaries of pump technology, they are poised to remain at the forefront of the industry for years to come.In conclusion, the Canned Motor Pump represents the future of pump technology, offering unparalleled efficiency, reliability, and safety for a wide range of industries. With a focus on innovation, quality, and customer support, the company behind this technology has solidified its position as a leader in the pumping industry. As businesses continue to seek more sustainable and cost-effective solutions, the Canned Motor Pump stands out as a game-changing technology that delivers on all fronts.
High-Performance Submersible Sewer Pumps for Efficient Wastewater Management
Certainly! Please provide the specific news content about the Submersible Sewer Pump and the company introduction you'd like me to use in crafting the 800-word news article.
Chemical Process Pump: Key Features and Applications
Certainly! Please provide the specific news content about the Chemical Process Pump and the company introduction you'd like me to use. Once I have those details, I can draft the 800-word news article for you.
High-Performance Horizontal Centrifugal Water Pump for Efficient Fluid Handling
Certainly! Please provide the specific news content about the Horizontal Centrifugal Water Pump and the company introduction you would like included. Once I have those details, I can draft an 800-word news article for you without any brand names.
High-Quality Chemical Process Pumps for Industrial Use
Chemical Process Pump Company Sets New Industry StandardChemical Process Pump Company, a leading manufacturer in the chemical process pump industry, is proud to announce the launch of their latest product that sets a new standard for efficiency and performance in the industry. With over 30 years of experience in designing and manufacturing high-quality chemical process pumps, the company has once again demonstrated their commitment to innovation and excellence.The new product features state-of-the-art technology that has been meticulously designed and tested to ensure reliable and efficient operation in the most demanding chemical process applications. This advanced pump offers industry-leading efficiency and performance, making it the ideal choice for a wide range of chemical process applications, including chemical manufacturing, petrochemical processing, pharmaceutical production, and more.The key to the exceptional performance of the new pump lies in its innovative design and construction. The pump is engineered using the latest materials and manufacturing techniques, resulting in a product that delivers superior reliability, durability, and efficiency. With a focus on sustainability and environmental responsibility, the company has also implemented energy-efficient features in the design of the pump, making it a cost-effective and environmentally friendly choice for chemical process operations.In addition to its cutting-edge technology, the new pump is also backed by the company's commitment to customer satisfaction and product support. Chemical Process Pump Company is dedicated to providing the highest level of service to its customers, offering comprehensive technical support, installation assistance, and maintenance services to ensure that their products continue to perform at their best for years to come. This commitment to customer satisfaction is a core value of the company, and it is reflected in every aspect of their business, from product design to customer service."We are thrilled to introduce our latest chemical process pump, which we believe sets a new standard for performance and efficiency in the industry," said the company's CEO. "Our team has worked tirelessly to develop a product that not only meets the current needs of our customers but also anticipates the future demands of the industry. We are confident that this new pump will provide unparalleled value to our customers and help them achieve their operational goals with maximum efficiency and reliability."Chemical Process Pump Company has a long-standing reputation for excellence in the chemical process pump industry, having established themselves as a trusted and reliable partner for companies around the world. Their products are known for their quality, performance, and durability, and the company's dedication to innovation and continuous improvement has earned them a leading position in the market.As the industry continues to evolve and adapt to new challenges and opportunities, Chemical Process Pump Company remains committed to staying at the forefront of technological advancements and industry best practices. The launch of their latest chemical process pump is a testament to this commitment, and the company looks forward to continuing to provide cutting-edge solutions to their customers in the years to come. With a focus on excellence, innovation, and customer satisfaction, Chemical Process Pump Company is poised to set new industry standards and lead the way towards a more efficient and sustainable future for chemical process operations.