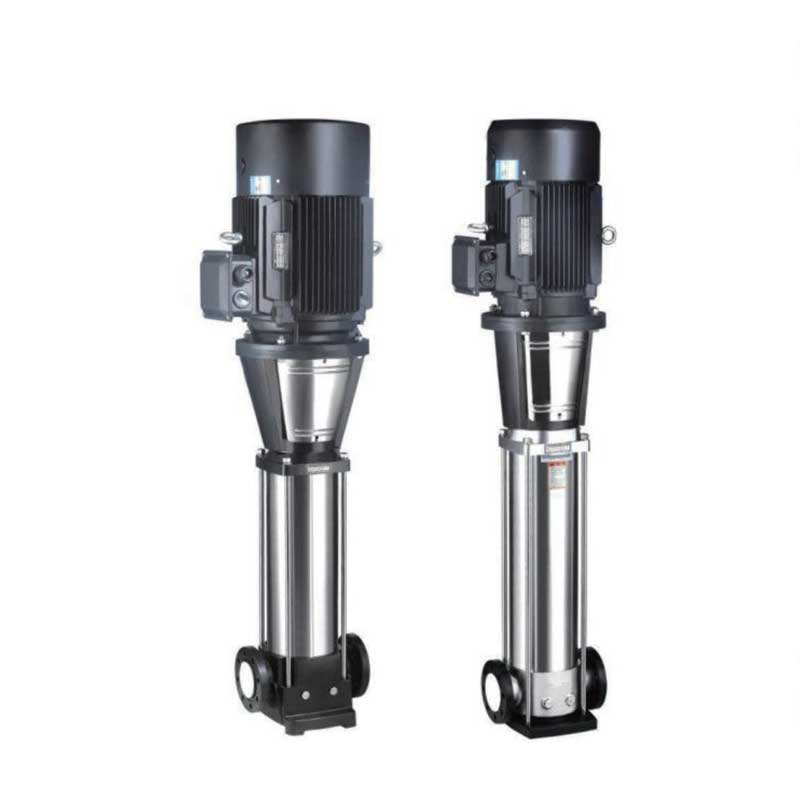
**Innovative Solutions in Fluid Handling: Advancements in Single Stage Single Suction Chemical Pumps**In the ever-evolving landscape of industrial fluid handling, the demand for reliable, efficient, and robust pumping solutions continues to grow. Single stage single suction chemical pumps have emerged as a pivotal component in meeting these industry requirements, offering streamlined performance and enhanced operational efficiency across a multitude of applications. This news article explores the latest advancements in single stage single suction chemical pumps, highlighting their critical role in chemical processing industries, and providing insights into the company that continues to lead innovation in this field.### The Role of Single Stage Single Suction Chemical PumpsChemical pumps are designed to transport aggressive, corrosive, and hazardous fluids safely and reliably. Within this category, single stage single suction centrifugal pumps hold a distinguished place due to their simplicity, ease of maintenance, and cost-effectiveness. They are widely used for transferring chemicals in industries such as petrochemical processing, pharmaceuticals, water treatment, and food manufacturing.Single stage pumps operate with a single impeller that imparts kinetic energy to the fluid, causing it to move through the pump casing. The single suction aspect refers to fluid entering the impeller eye from one side, simplifying the flow pattern and reducing mechanical complexity. This configuration is especially advantageous in applications where moderate pressure and flow rates are required, enabling both versatility and operational reliability.### Latest Industry DevelopmentsRecent technological advances in materials science and pump design have significantly boosted the capabilities of single stage single suction chemical pumps. Manufacturers are now integrating corrosion-resistant alloys, advanced sealing technologies, and optimized hydraulic components. Such enhancements ensure longer service life, minimal downtime, and improved safety for handling aggressive chemicals.Innovative design methodologies have also improved the pumps’ efficiency, reducing energy consumption without compromising performance. Computational fluid dynamics (CFD) modeling enables precise impeller and casing configurations tailored to specific chemical properties and flow regimes. These data-driven improvements lead to reduced cavitation risks—a common challenge in chemical pumping—thus safeguarding operational integrity.Moreover, modern pumps boast compliance with stringent environmental and safety regulations. Leakage prevention and minimized emissions are at the core of new designs, supported by enhanced mechanical seals and secondary containment features. Such innovations reflect the industry’s commitment to sustainable and responsible chemical processing.### Versatile Applications Across IndustriesThe adaptability of single stage single suction chemical pumps makes them indispensable across various sectors:- **Chemical Manufacturing:** Efficient transfer of acids, alkalis, solvents, and corrosive intermediates.- **Water and Wastewater Treatment:** Handling of chemicals for disinfection, pH adjustment, and sludge processing.- **Pharmaceutical Production:** Precise dosing and transfer of sensitive chemical solutions under hygienic conditions.- **Food and Beverage:** Safe handling of cleaning agents and food-grade chemicals.- **Petrochemical Refining:** Transportation of hydrocarbon fluids with high chemical resistance requirements.The pumps’ straightforward construction combined with customizable material options enables tailored solutions meeting stringent process requirements.### Company Insights: Excellence in Chemical Pump InnovationAt the forefront of delivering advanced pumping solutions is [Company Name], a leader renowned for its commitment to quality, innovation, and customer-centric engineering. With decades of industry experience, [Company Name] has specialized in designing and manufacturing chemical pumps that address the unique challenges of fluid handling in harsh environments.The company’s comprehensive product range includes single stage single suction pumps engineered for diverse chemical applications. Leveraging state-of-the-art research facilities and a skilled engineering workforce, [Company Name] emphasizes bespoke designs to improve operational efficiency and reduce lifecycle costs for clients worldwide.Customer collaboration is pivotal to their approach. From initial consultation through installation and after-sales service, [Company Name] ensures that each pump solution aligns perfectly with process variables, safety standards, and maintenance protocols. Their global footprint and localized support capabilities further cement their leadership position in the chemical pump market.### Commitment to Sustainability and InnovationRecognizing the increasing focus on sustainable industrial practices, [Company Name] dedicates significant resources to developing eco-friendly pump technologies. This includes optimizing pump hydraulics for energy savings, adopting environmentally safe materials, and enhancing system integration for smart operation and predictive maintenance.Ongoing research partnerships with academic and industrial entities ensure that [Company Name] remains at the cutting edge of fluid dynamics innovation and chemical compatibility. Their pursuit of excellence translates into pumps that not only perform reliably but also contribute to broader goals of environmental stewardship and industrial safety.### ConclusionSingle stage single suction chemical pumps continue to be indispensable tools in the chemical processing industry, offering an optimal balance of simplicity, durability, and cost efficiency. As advancements in pump technology and materials evolve, these pumps are becoming more reliable, efficient, and environmentally responsible.With [Company Name] leading the charge in innovative pump design and customer-focused solutions, industries worldwide can rely on these pumps to meet demanding chemical handling needs safely and effectively. The future of fluid handling looks promising, empowered by continuous improvement and dedicated expertise in pump technology.For more information on single stage single suction chemical pumps and customized fluid handling solutions, please contact [Company Name] or visit their official website.---*Note: Brand names have been intentionally omitted to maintain neutrality and focus on product and technology features.*
Read More