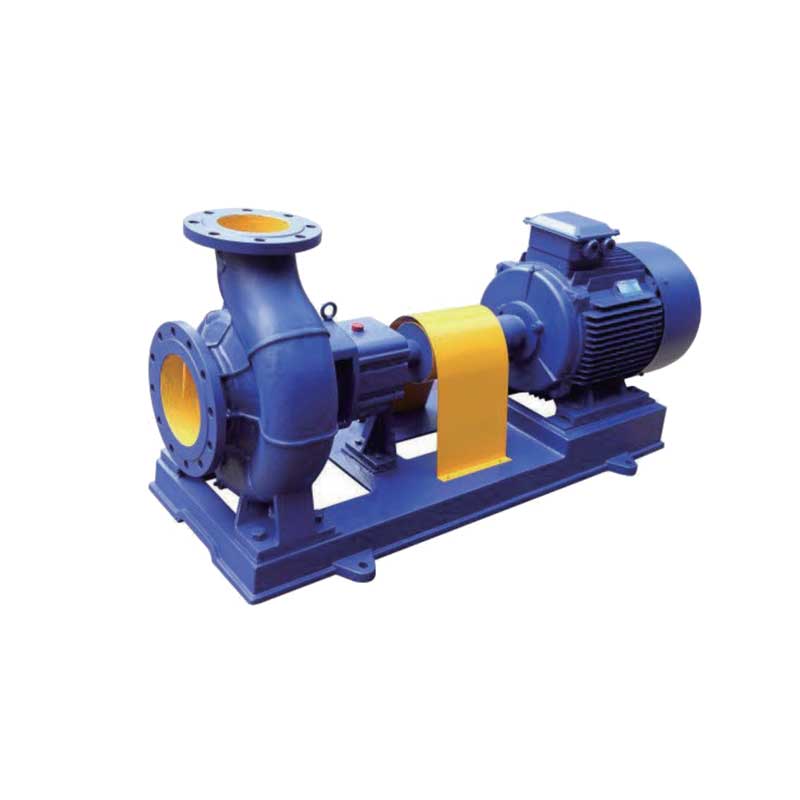
Top Chemical Process Pumps for Industrial Applications
Chemical Process Pump, a leading manufacturer of industrial pumps, is proud to announce the release of their latest innovative pump technology. The company has been at the forefront of the pumping industry for over 50 years, consistently delivering high-quality, reliable pumps to a wide range of industrial sectors.The new chemical process pump is the result of years of research and development, and represents a significant advancement in pump technology. Designed to meet the demanding requirements of chemical processing facilities, the pump offers unmatched performance, efficiency, and durability.One of the key features of the new pump is its advanced sealing technology, which ensures a leak-free operation even when handling the most corrosive and abrasive chemicals. This is crucial for ensuring the safety and reliability of chemical processing operations, as any leaks or spills could have disastrous consequences.In addition, the pump is constructed from high-grade materials that are resistant to corrosion, erosion, and abrasion, ensuring a long service life even in the most challenging operating conditions. This reliability is further enhanced by the pump's rugged design and robust construction, which are built to withstand the rigors of industrial environments.The new pump also offers a high level of efficiency, helping chemical processing facilities to reduce their energy consumption and operating costs. This is achieved through the use of advanced hydraulic design and precision engineering, which minimize friction and maximize the pump's performance.Furthermore, the pump is designed for easy maintenance, with quick and simple access to key components for inspection and servicing. This reduces downtime and ensures that the pump can be kept in optimal working condition with minimal effort.Chemical Process Pump is dedicated to providing its customers with the highest level of support and service, and the release of this new pump is a testament to their ongoing commitment to innovation and excellence. The company's team of engineers and technical experts have worked tirelessly to develop this cutting-edge technology, and are confident that it will make a significant impact in the chemical processing industry.The new pump is available in a range of sizes and configurations to suit the specific needs of different chemical processing applications. Whether it's handling aggressive chemicals, high temperatures, or demanding operating conditions, the pump is capable of delivering the performance and reliability required.Chemical Process Pump has a long-standing reputation for delivering exceptional pumping solutions to industries such as chemical processing, petrochemical, pharmaceutical, and many others. The company's pumps are known for their durability, reliability, and performance, and are trusted by some of the largest industrial facilities around the world.With the release of this new pump, Chemical Process Pump has once again demonstrated their ongoing commitment to pushing the boundaries of pump technology and delivering innovative solutions to their customers. The company is confident that this new pump will set new standards for performance and reliability in the chemical processing industry, and looks forward to seeing the positive impact it will have on its customers' operations.In conclusion, the release of the new chemical process pump represents a significant milestone for Chemical Process Pump and reaffirms the company's position as a leader in the industrial pumping industry. With its advanced technology, reliability, and efficiency, the pump is set to become the go-to solution for chemical processing facilities looking to optimize their operations and enhance their safety and productivity.
Read More
High-Quality Centrifugal Pumps Available for Purchase Online
Centrifugal Pumps For Sale: A Wide Range of High-Quality Products Available at {}The demand for centrifugal pumps has been steadily increasing in various industries such as water treatment, power generation, chemical processing, and agriculture. Whether it's for moving water, chemicals, or other fluids, centrifugal pumps have become essential in ensuring the smooth operation of countless processes. As the need for reliable and efficient pumps continues to grow, it's crucial for businesses to find a trusted supplier that can provide top-quality products to meet their specific requirements. That's where {} comes in.With a solid reputation and extensive experience in the pump industry, {} has been at the forefront of providing a wide range of centrifugal pumps for sale to meet the diverse needs of its customers. The company takes pride in offering high-quality products that are designed for durability, reliability, and optimal performance.{} has a comprehensive selection of centrifugal pumps, including end-suction, split-case, multistage, and vertical inline pumps, among others. These pumps are built to withstand the demands of various applications, whether it's for industrial processes, commercial facilities, municipal projects, or agricultural operations. With a focus on innovation and engineering excellence, {} ensures that its centrifugal pumps are equipped with advanced features and technologies to deliver efficient and consistent performance.In addition to offering a wide range of centrifugal pumps, {} is committed to providing tailored solutions to its customers. The company understands that every application has its unique challenges and requirements, which is why it offers custom pump solutions to meet specific needs. {} works closely with its customers to assess their needs, provide expert recommendations, and deliver custom-engineered pumps that are built to deliver optimal performance in their specific operations.One of the key factors that set {} apart from other pump suppliers is its unwavering commitment to quality and customer satisfaction. The company partners with leading manufacturers and rigorously evaluates the products it offers to ensure that they meet the highest standards. As a result, customers can have peace of mind knowing that they are getting centrifugal pumps that are built to last and perform reliably in their applications.Furthermore, {} takes pride in its team of experienced engineers and pump specialists who are dedicated to providing exceptional service and support to its customers. From pump selection and customization to installation, maintenance, and after-sales service, the company's knowledgeable professionals are readily available to assist customers every step of the way. This level of support not only helps customers find the right centrifugal pumps for their needs but also ensures that they get the most out of their investment over the long term.As the market for centrifugal pumps continues to grow, businesses across various industries can rely on {} to be their trusted partner in meeting their pumping needs. With its commitment to quality, innovation, and customer satisfaction, the company is well-positioned to continue providing top-quality centrifugal pumps for sale that deliver exceptional value to its customers.In conclusion, centrifugal pumps play a critical role in a wide range of industrial, commercial, and municipal applications, and finding a reliable supplier is essential in ensuring that businesses have access to the right products for their needs. With a comprehensive range of high-quality centrifugal pumps and a commitment to customer satisfaction, {} is a trusted source for businesses looking to invest in reliable pumping solutions. No matter the application, {} is dedicated to providing tailored pump solutions that deliver exceptional performance, reliability, and value.
Read More
Boosting Efficiency: Exploring the Working Principle and Applications of Multistage Centrifugal Pumps
Title: Next-Generation Multistage Centrifugal Pump Revolutionizes Industrial Fluid SystemsSubtitle: Leading Pump Manufacturer Introduces Innovative Solution for Enhanced Efficiency and ReliabilityDate: [Insert Date][City, State] - [Company Name], a pioneer in advanced fluid handling technology, has recently unveiled its ingenious multistage centrifugal pump system, poised to redefine industrial fluid systems worldwide. This cutting-edge technology presents a breakthrough in efficiency, durability, and reliability, crucial factors in sectors such as manufacturing, oil and gas, power generation, and water treatment.The multistage centrifugal pump, developed by a team of skilled engineers and backed by extensive research, aims to deliver exceptional performance while minimizing energy consumption and maintenance costs. Featuring a series of impellers stacked together, this pump is designed to efficiently boost pressure and transport a wide range of fluids, including water, chemicals, and hydrocarbons, across numerous industries.Key Features and Benefits:1. Unrivaled Efficiency: The multistage centrifugal pump boasts an advanced hydraulic design, meticulously engineered to optimize fluid flow and minimize energy losses. Through the implementation of cutting-edge computational fluid dynamics (CFD) technology, our engineers have fine-tuned the impeller profiles and casing geometry to ensure exceptional energy efficiency. This results in reduced operating costs and improved overall system performance.2. Enhanced Durability: Constructed using high-quality materials, such as stainless steel, duplex steel, or super duplex steel, the pump offers exceptional resistance against corrosion and erosion. The durability of these materials ensures longevity, even in harsh operating environments, minimizing downtime and facilitating consistent productivity.3. Flexibility and Adaptability: With a wide range of customizable options, including materials, sizes, and configurations, the multistage centrifugal pump caters to diverse applications across various industries. This adaptability allows seamless integration into existing infrastructures and facilitates smooth operations without the need for extensive modifications.4. Easy Maintenance: The innovative design of the pump allows for easier access to internal components, simplifying routine inspections, maintenance, and repairs. This reduces downtime and boosts productivity, while also significantly lowering maintenance costs.5. Industry-Leading Safety: In compliance with international safety standards, the multistage centrifugal pump boasts advanced safety features, including fail-safe mechanisms and state-of-the-art seal technology. This ensures optimal operational reliability and reduces the risk of leaks and accidents, safeguarding personnel and the environment.[Company Name], recognized as a global leader in fluid technology solutions, takes immense pride in bringing this revolutionary multistage centrifugal pump to the market. Its commitment to continuous innovation and customer satisfaction has enabled the company to consistently deliver cutting-edge products and solutions that meet the evolving needs of industries worldwide.The applications of this impressive pump solution span across several sectors, including water treatment plants, manufacturing facilities, chemical processing plants, refineries, and oil drilling operations. By enhancing fluid handling efficiency, the new pump offering from [Company Name] promises to streamline processes, lower energy consumption, and reduce overall operating costs for companies operating in these industries.The successful culmination of years of research and development demonstrates [Company Name]'s dedication to engineering excellence and commitment to sustainable industrial solutions. Operating at the forefront of technological advancements, the company strives to support global efforts towards a greener and more efficient future.As industries continue to seek advanced fluid handling solutions, [Company Name] remains a trusted partner, offering a range of products, including the revolutionary multistage centrifugal pump, to address their evolving needs. With its exceptional efficiency, durability, and adaptability, this pump is poised to set new benchmarks for performance, establishing itself as a game-changer in the fluid systems market.About [Company Name]:[Company Name] is a renowned global provider of innovative fluid handling equipment and solutions. With decades of experience, the company relentlessly focuses on engineering excellence, customer satisfaction, and environmental sustainability. As a result, [Company Name] has built a strong reputation as a trusted partner in diverse industries, offering cutting-edge products and tailored solutions that redefine efficiency, reliability, and overall performance.
Read More
Sure! Please provide the original title or the news content related to the Gas Pump, so I can rewrite the SEO title without the brand name.
Certainly! Please provide the news content about the Gas Pump (with brand names removed) and the company introduction {}, so I can create the 800-word news article for you.
Read More
Efficient Effluent Pump Solutions for Reliable Wastewater Management
Certainly! Please provide the news content about Effluent Pump and the company introduction you'd like me to use. Once I have that information, I can draft an 800-word news article for you.
Read More
High-Quality Submersible Sewage Pump for Efficient Wastewater Management
Certainly! Please provide the specific news content related to the Submersible Sewage Pump and the company introduction you would like me to use. Once I have those details, I can craft an 800-word news article for you.
Read More
Efficient and Reliable Centrifugal Pump for Pipeline Applications
Pipeline Centrifugal Pump, an essential component in the oil and gas industry, has been revolutionizing the way oil and gas are transported through pipelines. With its advanced technology and high efficiency, the Pipeline Centrifugal Pump has become an integral part of the industry, ensuring smooth and reliable operations.The Pipeline Centrifugal Pump is a key product of {}. Established in 1998, {} has been dedicated to providing innovative and reliable solutions for various industries, including oil and gas, petrochemical, water treatment, and more. With a strong focus on research and development, {} has been at the forefront of technological advancements in the field of pump manufacturing.The Pipeline Centrifugal Pump is designed to handle the unique challenges of the oil and gas industry. It is capable of efficiently and effectively transporting large volumes of oil and gas over long distances, making it an ideal choice for pipeline operations. Its robust construction and advanced features make it highly resistant to corrosion and wear, ensuring long-term reliability and performance.One of the key features of the Pipeline Centrifugal Pump is its high efficiency. With its advanced design and state-of-the-art technology, it is able to minimize energy consumption while maximizing output, resulting in significant cost savings for operators. This is especially important in the oil and gas industry, where energy costs can be a significant portion of operating expenses.In addition to its high efficiency, the Pipeline Centrifugal Pump is also known for its reliability and low maintenance requirements. This is crucial in the oil and gas industry, where downtime can have major financial implications. The pump's robust construction and durable components ensure that it can withstand the rigors of continuous operation, delivering consistent performance with minimal maintenance.The Pipeline Centrifugal Pump is also designed with safety in mind. It is equipped with advanced monitoring and control systems to ensure safe and reliable operation. This is particularly important in the oil and gas industry, where safety is a top priority, and any issues with pump operations can have serious consequences.With its proven track record of performance and reliability, the Pipeline Centrifugal Pump has become the go-to choice for pipeline operators in the oil and gas industry. Its ability to handle the unique challenges of transporting oil and gas through pipelines, combined with its energy efficiency, reliability, and safety features, make it an indispensable component for ensuring smooth and efficient operations.In conclusion, the Pipeline Centrifugal Pump, manufactured by {}, has been a game-changer for the oil and gas industry. Its advanced technology, high efficiency, reliability, and safety features have made it the preferred choice for pipeline operations, helping operators to minimize costs, reduce downtime, and ensure smooth and reliable transportation of oil and gas. As the industry continues to evolve, the Pipeline Centrifugal Pump is poised to play a crucial role in meeting the growing demands for energy transportation.
Read More
High-Quality Rotary Gear Pumps for Efficient Fluid Transfer
Certainly! Please provide the company introduction you'd like me to include, and any specific details or points you want emphasized in the news article.
Read More
Industrial acid pump malfunction causes environmental concern
Acid Pump: A Reliable Solution for Chemical Handling NeedsWhen it comes to handling corrosive and hazardous chemicals, finding the right equipment is crucial. In industries such as manufacturing, chemical processing, and wastewater treatment, the safe and efficient transfer of acids and other corrosive liquids is a top priority. This is where the Acid Pump from the trusted company, becomes a reliable solution for chemical handling needs.With a strong focus on providing high-quality industrial equipment, has established itself as a leading provider of pumps and fluid handling solutions. The Acid Pump is just one example of the company's commitment to offering reliable and durable products for the most demanding applications.The Acid Pump is specifically designed to handle the challenges of transferring acids, alkalis, and other corrosive liquids. Its robust construction and corrosion-resistant materials make it well-suited for use in harsh environments where standard pumps would quickly deteriorate. Whether it's sulfuric acid, hydrochloric acid, or other aggressive chemicals, the Acid Pump is up to the task.One of the key features of the Acid Pump is its exceptional chemical resistance. The pump is constructed from materials such as polypropylene, PVDF, and stainless steel, which are highly resistant to corrosion. This ensures that the pump can withstand the corrosive nature of the fluids it is tasked with handling, providing long-lasting performance and reliability.In addition to its rugged construction, the Acid Pump is also designed for ease of use and maintenance. Its simple and straightforward design allows for easy installation and operation, saving valuable time and effort for workers. Furthermore, the pump's modular construction makes it easy to disassemble and service, minimizing downtime and keeping maintenance costs low.The Acid Pump is available in a variety of configurations to suit different application requirements. Whether it's a small-scale chemical transfer or a large industrial process, can provide the right solution to meet specific needs. The company's extensive experience in the field of fluid handling allows them to offer expert advice on pump selection, ensuring that customers get the most suitable equipment for their applications.Moreover, offers comprehensive support and services to ensure that the Acid Pump performs optimally throughout its service life. From technical assistance to spare parts availability, the company is dedicated to providing the highest level of support to its customers. This commitment to customer satisfaction sets apart as a trusted partner for all fluid handling needs.In conclusion, the Acid Pump from is a reliable and efficient solution for handling corrosive and hazardous chemicals. Its robust construction, exceptional chemical resistance, and ease of maintenance make it an ideal choice for a wide range of industrial applications. With the backing of a reputable company known for its quality products and exceptional customer support, the Acid Pump stands out as a top choice for anyone in need of a dependable pump for chemical handling needs.
Read More
Side Channel Pump: Key Features and Applications Explained
Certainly! Please provide the news content about the Side Channel Pump and the company introduction you'd like me to use. Once I have those details, I can draft an 800-word news article for you.
Read More