
Close Coupled Centrifugal Pump: Features, Benefits, and Applications
By:Admin
Company News & Blog
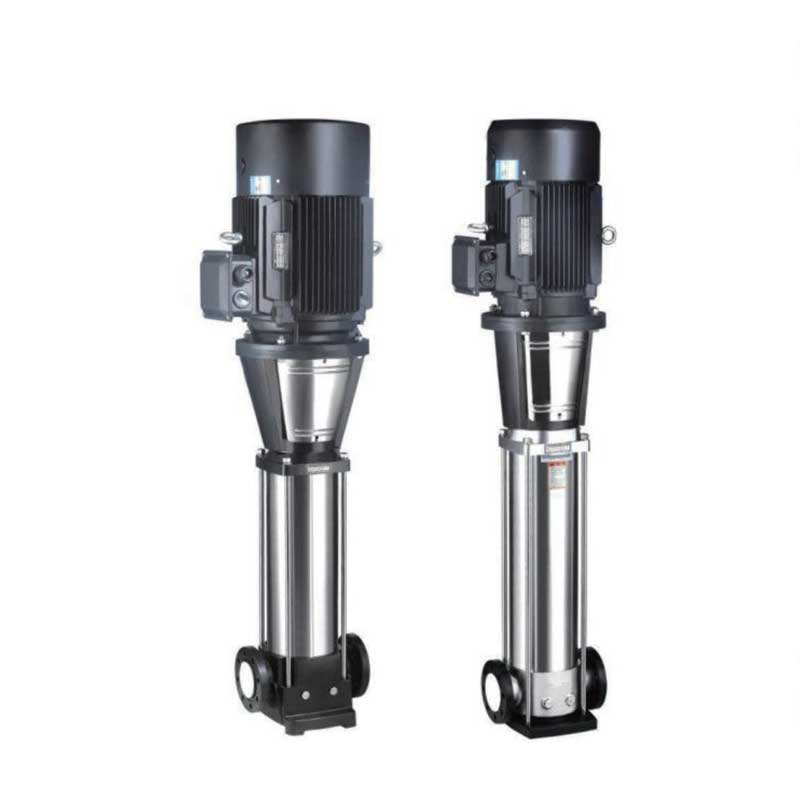
Close Coupled Centrifugal Pump: Efficient and Reliable Pumping Solution
Certainly! Please provide the news content regarding the Close Coupled Centrifugal Pump (without the brand name) and the company introduction {} so I can draft an 800-word news article for you.
High-Quality Multistage Pump Factory Offers Reliable Solutions
Dg Multistage Pump Factory, a leading manufacturer of industrial pumps, has been making waves in the industry with its innovative and high-quality products. With a strong focus on research and development, the company has cemented its position as a reliable and trusted supplier of multistage pumps for various applications.Established in [], Dg Multistage Pump Factory has grown from strength to strength, constantly evolving and adapting to meet the changing needs of its customers. The company has invested heavily in state-of-the-art manufacturing facilities, ensuring that its pumps are manufactured to the highest standards of quality and precision.Dg Multistage Pump Factory offers a wide range of multistage pumps, including [] series, [] series, and [] series. These pumps are designed to deliver exceptional performance, reliability, and efficiency, making them ideal for use in various industries such as [].One of the key factors that set Dg Multistage Pump Factory apart from its competitors is its commitment to innovation. The company has a dedicated team of engineers and researchers who are constantly working on developing new and improved pump technologies. This relentless pursuit of innovation has allowed Dg Multistage Pump Factory to stay ahead of the curve and provide its customers with cutting-edge pump solutions.In addition to its focus on innovation, Dg Multistage Pump Factory also places a strong emphasis on customer satisfaction. The company works closely with its clients to understand their specific needs and requirements, and then provides customized pump solutions to meet those needs. This customer-centric approach has earned Dg Multistage Pump Factory a reputation for being a responsive and reliable partner.Furthermore, Dg Multistage Pump Factory is committed to upholding the highest standards of quality and reliability in all its products. The company works in compliance with [] standards and holds various certifications that attest to the quality of its pumps. This commitment to quality has earned Dg Multistage Pump Factory the trust and loyalty of its customers.Moreover, Dg Multistage Pump Factory places a strong emphasis on sustainability and environmental responsibility. The company is constantly exploring ways to make its manufacturing processes more environmentally friendly and is committed to reducing its environmental impact. This commitment to sustainability aligns with the company's values and resonates with customers who are increasingly mindful of the environmental impact of the products they use.Looking ahead, Dg Multistage Pump Factory is poised for continued success and growth. The company has ambitious plans to expand its product range, enter new markets, and further strengthen its position as a leader in the industry. With its unwavering commitment to innovation, quality, and customer satisfaction, Dg Multistage Pump Factory is well-equipped to meet the evolving needs of its customers and remain a trusted partner for all their pump requirements.
Delicious Chocolate Pump: The Ultimate Indulgence for Chocolate Lovers
A new and innovative product has been making waves in the confectionery industry, marking a significant advancement in chocolate production. The Chocolate Pump, created by an industry-leading company, is set to revolutionize the way chocolate is made and enjoyed.The Chocolate Pump, developed by the anonymous company, is a state-of-the-art machine that automates the process of creating delectable and smooth chocolate. This innovative equipment is designed to efficiently process cocoa beans and other ingredients, while maintaining the highest quality of chocolate.The company behind this groundbreaking invention is known for its dedication to excellence and commitment to enhancing the confectionery industry. With a solid reputation for creating cutting-edge technologies, the company has built a strong presence in the market, catering to the needs of chocolatiers and confectioners worldwide.The Chocolate Pump is expected to streamline the chocolate production process, offering a cost-effective solution while ensuring superior quality. The machine is equipped with advanced features that enable precise control over the refining and conching stages, resulting in a consistent and velvety texture in the finished product.Furthermore, the Chocolate Pump is designed with sustainability in mind, incorporating energy-efficient mechanisms and reducing waste in the production process. This aligns with the company's commitment to environmental responsibility, embracing eco-friendly practices in its operations.In addition to its technical advancements, the Chocolate Pump showcases a user-friendly interface, making it accessible to chocolatiers of all skill levels. Its intuitive design and automated functions allow for greater efficiency and productivity, ultimately benefiting businesses in the confectionery sector.The anonymous company has received widespread acclaim for its innovative approach to chocolate manufacturing, with industry experts lauding the Chocolate Pump for its potential to revolutionize the way chocolate is produced. By streamlining the traditional methods and enhancing the overall quality, this new equipment is poised to set a new standard in the confectionery industry.The company's dedication to research and development has paved the way for the creation of the Chocolate Pump, setting a precedent for future advancements in chocolate production. With a focus on precision engineering and technological innovation, the company continues to push the boundaries of what is possible within the confectionery sector.As the demand for high-quality chocolate continues to rise, the introduction of the Chocolate Pump comes at a pivotal time, offering a solution that addresses the evolving needs of the industry. Its potential to increase efficiency and consistency in chocolate production is set to have a profound impact on businesses and consumers alike.The company's commitment to excellence and ingenuity has solidified its position as a leader in the confectionery industry, with the Chocolate Pump standing as a testament to its dedication to advancing the craft of chocolate making. With its innovative design and unparalleled capabilities, the Chocolate Pump is poised to shape the future of chocolate production, setting a new standard for quality and efficiency.
High-Powered Water Pump for Jet Engines: The Latest Technology in Water Pumping Systems
The Water Pump Company is proud to introduce its latest innovation in water pump technology - the Jet Water Pump. This state-of-the-art pump is designed to provide superior performance and reliability for a wide range of water pumping applications.The Jet Water Pump is a powerful and efficient pump that is capable of delivering high volumes of water at high pressures. It is equipped with a durable and corrosion-resistant construction, making it suitable for use in a variety of environments, including residential, commercial, and agricultural settings.One of the key features of the Jet Water Pump is its innovative jet system, which allows it to achieve high levels of efficiency and performance. This system is designed to optimize water flow and pressure, ensuring that the pump can deliver a consistent and powerful performance.In addition to its superior performance, the Jet Water Pump is also designed with user convenience in mind. It is equipped with a user-friendly control panel that allows for easy operation and customization of water pumping settings. This makes it easy for users to adjust the pump to meet their specific water pumping needs.The Water Pump Company is known for its commitment to quality and innovation, and the Jet Water Pump is a testament to this dedication. The company has invested heavily in research and development to ensure that its products are at the forefront of water pump technology. As a result, the Jet Water Pump boasts a combination of cutting-edge technology and reliable, durable construction.The Jet Water Pump is backed by the company's comprehensive customer support and service network. The Water Pump Company is committed to providing its customers with the support they need to get the most out of their water pump. Whether it's installation, maintenance, or troubleshooting, the company's team of experts is available to provide assistance and ensure that the Jet Water Pump performs at its best.The launch of the Jet Water Pump represents a significant milestone for the Water Pump Company. It underscores the company's ongoing commitment to delivering high-quality, high-performance products to its customers. With its innovative design, powerful performance, and user-friendly features, the Jet Water Pump is poised to set new standards in the water pump industry."We are thrilled to introduce the Jet Water Pump to the market," said a spokesperson for the Water Pump Company. "This pump represents the culmination of years of research and development, and we believe it will make a significant impact in the industry. We are confident that our customers will be impressed by its performance and reliability."The Jet Water Pump is now available for purchase through the Water Pump Company's network of authorized dealers and distributors. With its unparalleled performance and durability, it is sure to become the go-to choice for anyone in need of a high-quality water pump.For more information about the Jet Water Pump and the Water Pump Company's full range of products and services, visit their website or contact their customer service team.
High Capacity Centrifugal Water Oil Pump for Efficient Industrial Use
A leading manufacturer in the field of pumps, Company X, has recently introduced a groundbreaking product - the Large Flow Rate Centrifugal Water Oil Pump. This new pump boasts a high capacity and efficiency, making it an ideal choice for a wide range of industrial applications.The Large Flow Rate Centrifugal Water Oil Pump is designed to handle large volumes of water and oil, making it perfect for industries such as petroleum, chemical, and water treatment. With a flow rate of up to 5000 cubic meters per hour, this pump is able to handle large-scale operations with ease. Its high efficiency also means that it is able to move large volumes of liquid with minimal energy consumption, making it a cost-effective solution for industrial pumping needs.In addition to its impressive performance, the Large Flow Rate Centrifugal Water Oil Pump is also built to last. The pump is constructed from high-quality materials and is designed to withstand the rigors of industrial use. This means that it is able to operate reliably and consistently, even in demanding environments. The pump is also easy to maintain, with simple and accessible components that make servicing and repairs a straightforward task.The introduction of the Large Flow Rate Centrifugal Water Oil Pump is a testament to Company X's commitment to innovation and excellence in the field of pumping technology. With a history of over 50 years in the industry, Company X has earned a reputation for producing high-quality and reliable pumping solutions. The company's team of engineers and experts have worked tirelessly to develop this new pump, drawing on their extensive knowledge and experience to create a product that meets the needs of modern industry.In addition to the Large Flow Rate Centrifugal Water Oil Pump, Company X offers a comprehensive range of pumping solutions for various industries and applications. From centrifugal pumps to submersible pumps, the company's product lineup is designed to cater to a wide range of needs. Company X also provides tailored solutions for specific requirements, working closely with clients to develop custom pumping solutions that meet their unique needs.Company X's dedication to customer satisfaction extends beyond the quality of its products. The company is known for its exceptional customer service, providing comprehensive support and assistance to clients at every step of the process. From initial consultation and product selection to installation and maintenance, Company X is committed to ensuring that its clients have a positive experience and achieve the best results with their pumping solutions.Looking ahead, Company X continues to invest in research and development, constantly seeking new and innovative solutions to meet the evolving needs of industry. The introduction of the Large Flow Rate Centrifugal Water Oil Pump is just one example of the company's ongoing commitment to advancing pumping technology and providing cutting-edge solutions.In conclusion, the introduction of the Large Flow Rate Centrifugal Water Oil Pump represents a significant milestone for Company X and a major development in the field of industrial pumping technology. With its impressive performance, reliability, and efficiency, this new pump is set to make a significant impact in a wide range of industries. Company X's dedication to innovation and customer satisfaction ensures that it will continue to be a leading force in the field of pumping technology for many years to come.
Powerful and Reliable Fire Fighting Pumps: Enhancing Safety and Protection
Title: Cutting-Edge Firefighting Pump Revolutionizes Fire Safety MeasuresIntroduction:In a notable development that promises to enhance fire safety measures globally, a renowned company has introduced an innovative firefighting pump. With its state-of-the-art technology and impressive functionality, this groundbreaking device seeks to redefine the way fires are tackled and revolutionize firefighting efforts worldwide. By combining cutting-edge engineering with a deep commitment to public safety, this revolutionary pump marks a significant milestone in the realm of fire protection.[CompanyName], a leader in the fire safety industry, has tirelessly worked towards evolving firefighting techniques and equipment. With their latest creation, the new firefighting pump sets new standards by offering unparalleled performance, utmost reliability, and ease of use. Designed to handle exigent firefighting scenarios, this advanced pump is set to transform how fire departments combat emergencies.Performance and Technological Advancements:The innovative firefighting pump from [CompanyName] boasts outstanding performance capabilities due to its groundbreaking technological advancements. Equipped with an intuitive interface, it ensures ease of operation and seamless integration with existing firefighting apparatus. This facilitates a smooth transition for experienced firefighters while reducing the training time required for inexperienced users.The pump's exceptional power and capacity allow it to discharge an impressive volume of water laced with firefighting agents, quelling flames effectively and efficiently. Moreover, its cutting-edge nozzle design enables precise targeting of water streams, enhancing its firefighting capabilities in densely populated areas or confined spaces where precision is of utmost importance.Durability and Reliability:Built with robust materials, the firefighting pump is engineered to withstand extreme temperatures, rugged terrain, and harsh operating conditions. Its superior durability and reliability make it a resilient asset for firefighting professionals, bolstering their confidence during critical emergency situations. The pump's low maintenance requirements and extended service life ensure cost-effectiveness, making it an ideal long-term investment for fire departments.Versatility and Customization:Recognizing the diverse needs of firefighting operations, [CompanyName] has designed its pump to be highly customizable. Varied options and configurations allow firefighting professionals to tailor the device to specific requirements. From adjustable flow rates and foam induction capabilities to optional auxiliary functions, the pump can be adapted swiftly to address different scenarios, optimizing response times and fire suppression efforts.Industry Collaboration and Robust Support:[CompanyName] understands the importance of collaboration and cooperation between fire departments, industry experts, and other stakeholders in the field of fire safety. By fostering strategic partnerships and actively engaging with the firefighting community, the company aims to continue advancing the technology and improving their product offerings.In addition to providing cutting-edge equipment, [CompanyName] emphasizes comprehensive support services, including maintenance and training programs. Their team of highly skilled technicians ensures efficient maintenance and repairs, empowering fire departments with uninterrupted access to their devices' top-notch performance.Conclusion:The introduction of this ground-breaking firefighting pump by [CompanyName] heralds a new era in fire safety and protection. With its exceptional performance, technological advancements, and robust design, this innovative device proves to be a game-changer in firefighting efforts worldwide. As fire departments worldwide strive to enhance their firefighting capabilities, this state-of-the-art pump promises to be a crucial tool, significantly improving response times, minimizing property damage, and, most importantly, saving lives.
Sewage Ejector Pump Cost: Comprehensive Pricing Guide and Factors Affecting Expenses
Certainly! Please provide me with the company introduction you would like to include in the news article, as well as the specific news content about Sewage Ejector Pump Cost that you want to base the article on. This will help me create a detailed and coherent 800-word news piece for you.
High-Quality Auto Water Pump: Everything You Need to Know
[Company Name], a leading provider of automotive parts and accessories, has recently announced the launch of a new and improved auto water pump. The company is known for its commitment to high-quality products and exceptional customer service, and this latest addition to their product lineup is sure to meet the needs of automotive enthusiasts and professionals alike.The new auto water pump from [Company Name] is designed to provide reliable and efficient cooling for a wide range of vehicle makes and models. With a focus on durability and performance, this water pump is built to withstand the rigors of daily driving and harsh operating conditions. Whether it’s for a passenger car, truck, or SUV, customers can trust that this pump will deliver the cooling power their vehicle needs.“We are thrilled to introduce our latest auto water pump to the market,” said [Spokesperson Name], a representative of [Company Name]. “At [Company Name], we are committed to offering top-of-the-line products that meet the highest standards of quality and reliability. This water pump is no exception – it’s been engineered to deliver exceptional performance and durability, ensuring that our customers can rely on it for years to come.”In addition to its robust construction, the new water pump from [Company Name] also features a number of design enhancements aimed at improving overall efficiency. This includes advanced impeller technology for increased water flow, as well as precision bearings for smooth and reliable operation. These features work together to promote optimal engine cooling, helping to prevent overheating and maintain proper operating temperatures.Furthermore, this water pump is backed by [Company Name]’s industry-leading warranty and customer support. The company takes pride in standing behind its products and providing the assistance that customers need, should they have any questions or concerns. This level of commitment to customer satisfaction sets [Company Name] apart as a trusted source for automotive parts and accessories.With a strong focus on research and development, [Company Name] is constantly innovating and improving its product offerings. The launch of the new auto water pump is just one example of the company’s dedication to staying at the forefront of the automotive aftermarket industry. By leveraging the latest technologies and manufacturing processes, [Company Name] is able to deliver superior products that meet the evolving needs of consumers and automotive professionals.As the automotive industry continues to evolve, [Company Name] remains committed to providing solutions that support vehicle performance and reliability. The new auto water pump is a testament to this ongoing commitment, offering a combination of quality, performance, and value that customers can rely on.In conclusion, the introduction of the new auto water pump from [Company Name] is a significant development for automotive enthusiasts and professionals. With its durable construction, efficient design, and strong warranty coverage, this water pump is poised to become a go-to solution for those in need of reliable engine cooling. As [Company Name] continues to lead the way in the aftermarket automotive industry, customers can look forward to more innovative products that deliver on the company’s promise of quality and performance.
Top 5 Liquid Pumps for Efficient Fluid Transfer
Liquid Pump, a leading company in the manufacturing and distribution of industrial pumps, is proud to announce the launch of their latest innovation, the High-Performance Liquid Pump. This new addition to their extensive line of pump products promises to revolutionize the industry with its cutting-edge technology and unparalleled efficiency.The High-Performance Liquid Pump is designed to meet the growing demands of various industries, including oil and gas, chemical processing, water treatment, and more. Its advanced features and capabilities make it the ideal choice for handling a wide range of liquids, from corrosive chemicals to abrasive slurries. With a powerful motor and robust construction, this pump is built to deliver exceptional performance and durability in even the most challenging environments.One of the key highlights of the High-Performance Liquid Pump is its innovative design, which incorporates state-of-the-art engineering and materials to ensure maximum reliability and longevity. The pump is equipped with advanced sealing technology to prevent leaks and ensure a tight, secure seal, even when handling aggressive fluids. This feature is especially crucial for industries where safety and reliability are of utmost importance.In addition to its impressive performance, the High-Performance Liquid Pump also offers unmatched versatility and flexibility. With a wide range of available configurations, customers can customize the pump to meet their specific requirements, whether it's for high-pressure applications, high-temperature liquids, or specialized chemical handling. This level of customization sets the pump apart from its competitors, allowing customers to tailor the pump to their exact needs without compromising on performance or quality.Furthermore, the High-Performance Liquid Pump is engineered for easy maintenance and serviceability, minimizing downtime and maximizing operational efficiency. Its modular design and accessible components make it simple to inspect, repair, and replace parts as needed, reducing overall maintenance costs and ensuring optimal performance over the pump's lifespan.As a trusted leader in the industry, Liquid Pump has a longstanding reputation for delivering top-quality products and exceptional customer service. With a team of experienced engineers and technical experts, the company is committed to providing comprehensive support to its customers, from initial product selection and installation to ongoing maintenance and troubleshooting. This dedication to customer satisfaction has earned Liquid Pump a loyal customer base and a strong reputation as a reliable partner in the industry."We are thrilled to introduce the High-Performance Liquid Pump to the market," said [Spokesperson's name], [Job title] at Liquid Pump. "This innovative pump represents a significant milestone for our company and reaffirms our commitment to delivering cutting-edge solutions to our customers. We are confident that the High-Performance Liquid Pump will set a new standard for performance, reliability, and versatility in the industry."With the launch of the High-Performance Liquid Pump, Liquid Pump continues to solidify its position as a frontrunner in the industrial pump market. The company's dedication to innovation, quality, and customer satisfaction sets it apart as a leading provider of pump solutions for a wide range of applications. As industries continue to evolve and demand more sophisticated pump technologies, Liquid Pump remains at the forefront, driving progress and setting new benchmarks for excellence.
Hydraulic Transfer Pump: Efficient Fluid Handling Solutions
**Innovative Hydraulic Transfer Pump Revolutionizes Fluid Handling Solutions**In the ever-evolving landscape of industrial fluid management, the introduction of the latest Hydraulic Transfer Pump marks a significant milestone. Designed to enhance efficiency, reliability, and safety, this state-of-the-art pump is set to transform operations across multiple sectors including agriculture, chemical processing, and manufacturing.**Advanced Technology Meets Practical Design**The Hydraulic Transfer Pump stands out due to its robust engineering and user-centric design. Engineered to handle a wide range of fluids—from water and fuels to aggressive chemicals—this pump offers unparalleled versatility. Its hydraulic-driven mechanism ensures consistent power delivery even in challenging environments where electrical options may pose risks or limitations.One of the core advantages of this pump lies in its ability to operate seamlessly without direct electrical input, thus reducing the chance of sparks or electrical hazards. This feature is particularly crucial in volatile settings such as oil fields and chemical plants where safety cannot be compromised. Moreover, the pump’s design incorporates corrosion-resistant materials, extending its lifespan and reducing maintenance downtime.**Boosting Operational Efficiency**In industries where time and resource management are critical, the Hydraulic Transfer Pump delivers impressive performance metrics. With high flow rates and pressure capabilities, it accelerates transfer processes, enabling businesses to meet tight deadlines and maximize throughput. The pump’s simple yet effective hydraulic drive mechanism also minimizes energy consumption compared to traditional electric pumps, contributing to cost savings and sustainability goals.Additionally, the pump’s modular construction allows for easy integration into existing systems, granting companies the flexibility to upgrade their infrastructure without extensive overhauls. This adaptability makes it an attractive investment not only for new projects but also for retrofitting older facilities.**Company Introduction**Founded with a commitment to innovation and quality, the company behind this cutting-edge Hydraulic Transfer Pump has consistently pushed the boundaries of fluid technology. With decades of experience, the organization specializes in designing and manufacturing equipment that meets the highest industry standards. Their comprehensive portfolio spans pumps, mixers, and filtration systems tailored to diverse industrial applications.The company prides itself on a customer-centric approach, offering customized solutions and hands-on support. Their R&D team works closely with clients to develop products that address specific operational challenges, ensuring reliability and efficiency. Through continuous improvement and adherence to stringent quality controls, the company has established itself as a trusted partner worldwide.**Applications Across Industries**The versatility of the Hydraulic Transfer Pump makes it suitable for numerous applications:- **Agriculture:** Efficient irrigation water transfer, fertilizer and pesticide handling without risk of contamination.- **Chemical Processing:** Safe movement of corrosive or flammable liquids with reduced chance of leaks or spills.- **Oil and Gas:** Transfer of fuels and lubricants onsite, avoiding electrical hazards in explosive environments.- **Manufacturing:** Handling process fluids, coolants, and cleaning agents with minimal maintenance requirements.This broad applicability not only highlights the pump’s technical advantages but also its contribution to operational safety and environmental protection.**Commitment to Sustainability**Understanding the growing importance of sustainable operations, the company incorporates eco-friendly principles into product design. The hydraulic nature of the pump minimizes electrical use and burnouts, leading to lower energy demands. Furthermore, the use of durable materials reduces waste and replacement frequency.By supporting efficient fluid transfer processes, the pump helps reduce emissions related to fuel transfers and chemical leaks. This aligns with global efforts to promote greener industrial practices.**Customer Success Stories**Several clients have already reported transformative results after integrating the Hydraulic Transfer Pump into their workflows. One agricultural cooperative noted a 30% reduction in water transfer time, translating to increased crop yields and lower labor costs. A chemical processing plant highlighted improved safety records, attributing fewer incidents to the pump’s non-electrical operation and leak-resistant design.Such feedback reflects the tangible benefits and reliability the product offers, reinforcing its market position.**Future Prospects and Innovations**Looking ahead, the company continues to invest in research and development aimed at enhancing pump efficiency and expanding capabilities. Plans include smart monitoring systems that provide real-time performance data and predictive maintenance alerts, further minimizing downtime and operational risks.The company’s vision centers on delivering fluid handling solutions that not only meet but exceed customer expectations, adapting to evolving industrial challenges and technological advancements.**Conclusion**The introduction of this Hydraulic Transfer Pump represents a leap forward in fluid management technology. Its innovative hydraulic drive system, combined with durable construction and versatile applications, addresses key industry needs for safety, efficiency, and sustainability. Backed by a company renowned for excellence and customer focus, this pump is poised to become an essential tool across sectors demanding reliable fluid transfer solutions.As industries strive towards more efficient and safer operations, embracing such advanced equipment is a strategic step toward achieving long-term productivity and environmental goals. The Hydraulic Transfer Pump is not just a piece of machinery—it is a catalyst for enhanced industrial performance worldwide.