
Chemical Pump: Essential Guide to Types, Uses, and Maintenance
By:Admin
Company News & Blog
High Pressure Vane Pump for Efficient Fluid Power Applications
Certainly! Please provide the news content about the High Pressure Vane Pump (with the brand name removed) and the company introduction {} so that I can craft an 800-word news article for you.
High-Quality Sanitary Pumps for Your Business Needs
Sanitary Pump Company, a leading manufacturer of high-quality sanitary pumps, has recently announced the release of their latest innovative product. The new pump incorporates advanced technology and design to meet the specific needs of the food, pharmaceutical, and other sanitary processing industries.The new pump is designed to provide superior performance, reliability, and ease of maintenance. It is specifically engineered to meet the stringent sanitary standards required for the processing of food and pharmaceutical products, ensuring the highest levels of hygiene and product safety.Sanitary Pump Company has a long-standing reputation for delivering innovative and reliable pumping solutions to a wide range of industries. Their commitment to quality and customer satisfaction has made them a trusted partner for businesses around the world.With over 30 years of experience in the industry, Sanitary Pump Company has established itself as a leader in the design and manufacture of sanitary pumps. Their team of highly skilled engineers and technicians are dedicated to developing cutting-edge pumping solutions that meet the evolving needs of their customers.The new pump features a hygienic design with smooth surfaces and sanitary connections to prevent the buildup of bacteria and contaminants. This ensures that the pump can be easily cleaned and sterilized, meeting the strict hygiene requirements of the food and pharmaceutical industries.In addition to its advanced hygienic design, the new pump also incorporates state-of-the-art materials and construction techniques to ensure long-term reliability and performance. The pump is built to withstand the rigorous demands of sanitary processing, providing consistent and efficient operation over its operational lifespan.Sanitary Pump Company prides itself on its commitment to customer satisfaction and support. The company offers a comprehensive range of services, including technical support, maintenance, and spare parts availability, to ensure that their customers can rely on their pumping solutions day in and day out.The release of the new pump demonstrates Sanitary Pump Company's ongoing dedication to innovation and excellence. The company's investment in research and development has resulted in a pump that not only meets the current industry standards but also anticipates the future needs of the sanitary processing industries."We are thrilled to introduce our latest sanitary pump to the market," said the CEO of Sanitary Pump Company. "This new product represents the culmination of our ongoing commitment to delivering the highest quality pumping solutions to our customers. We believe that this pump will set new standards for performance and reliability in the food and pharmaceutical processing industries."The new pump is now available for purchase, and Sanitary Pump Company is actively working with customers to integrate it into their processing operations. With its advanced features and superior performance, the new pump is expected to make a significant impact on the sanitary processing industry.Sanitary Pump Company continues to lead the way in the development of innovative pumping solutions for the food, pharmaceutical, and other sanitary processing industries. With their latest release, they are poised to further solidify their position as a trusted partner for businesses seeking reliable and efficient pumping solutions.
Efficient Water Pump for Home Use
Water Pump Company Introducing Advanced Technology for More Efficient Water Management[City, Date] - As the global demand for clean and efficient water management continues to rise, Water Pump Company is proud to introduce its latest innovation in water pumping technology. With a strong commitment to sustainability and innovation, Water Pump Company is at the forefront of providing reliable and efficient solutions for water management across various industries.With over [number] years of experience in the industry, Water Pump Company has established a strong reputation for delivering high-quality and durable water pumping systems for a wide range of applications. From agricultural irrigation to municipal water supply, the company's products have been widely recognized for their performance and reliability.The latest addition to Water Pump Company's product lineup is the [model name], which incorporates advanced technology to deliver superior efficiency and performance. This cutting-edge water pumping system is designed to meet the growing demand for sustainable water management solutions, offering significant energy savings and reduced environmental impact."We are excited to introduce the [model name] to the market, as it represents a significant advancement in water pumping technology," said [Spokesperson's Name], CEO of Water Pump Company. "Our team has worked tirelessly to develop a solution that not only meets the needs of our customers but also contributes to a more sustainable future for water management."The [model name] incorporates state-of-the-art features, including precision-engineered components and advanced control systems, to optimize energy usage and ensure reliable operation. With a focus on efficiency and durability, this water pumping system is designed to withstand the rigors of continuous operation and provide long-term performance in demanding environments.In addition to its cutting-edge technology, the [model name] also reflects Water Pump Company's commitment to sustainability. The system is designed to minimize water wastage and reduce the overall environmental impact of water management processes. By optimizing resource utilization and reducing energy consumption, the [model name] contributes to a more sustainable approach to water pumping.Furthermore, Water Pump Company's dedication to customer satisfaction is evident in the comprehensive support and service offerings that accompany the [model name]. The company's team of experts is readily available to provide technical assistance, maintenance, and training to ensure that customers can maximize the performance and longevity of their water pumping systems.With its advanced technology, commitment to sustainability, and focus on customer satisfaction, Water Pump Company continues to set the standard for excellence in water management solutions. As the demand for efficient water pumping systems continues to grow, the introduction of the [model name] reaffirms the company's position as a leader in the industry."We are confident that the [model name] will make a significant impact on the way water is managed across various industries," added [Spokesperson's Name]. "We believe that this innovation will not only benefit our customers but also contribute to the global efforts to conserve and manage water resources more effectively."As Water Pump Company introduces its latest advancement in water pumping technology, it is clear that the company remains dedicated to driving innovation and sustainability in the water management industry. By leveraging advanced technology and a commitment to customer satisfaction, Water Pump Company is well positioned to meet the evolving needs of its customers and contribute to a more sustainable future for water management.
Top 5 Stainless Steel Hygienic Pumps for Sanitary Applications
Stainless Steel Hygienic Pump Revolutionizes the Food and Beverage IndustryIn today's rapidly growing food and beverage industry, ensuring the highest level of hygienic standards is paramount. With the increasing focus on food safety and quality, there is a growing demand for reliable and efficient hygienic pumps that can meet the rigorous requirements of the industry. This is where the Stainless Steel Hygienic Pump from [Company Name] comes into play, revolutionizing the way food and beverage processing is done.The Stainless Steel Hygienic Pump from [Company Name] is engineered to provide the highest level of hygiene and efficiency, making it the go-to solution for food and beverage processing companies. With its innovative design and advanced features, this pump is setting new standards in the industry.One of the key features of the Stainless Steel Hygienic Pump is its construction using high-quality stainless steel. This not only ensures the durability and longevity of the pump but also makes it highly resistant to corrosion, making it ideal for use in the food and beverage industry where hygiene is of utmost importance.The pump is also designed to meet the strictest hygienic standards, with a smooth, crevice-free design that eliminates any potential areas for bacterial growth or contamination. This makes it an ideal choice for handling food and beverage products, ensuring that the quality and safety of the products remain uncompromised throughout the processing.In addition to its hygienic design, the Stainless Steel Hygienic Pump is also highly efficient, delivering exceptional performance while minimizing energy consumption. This not only helps in reducing operational costs but also ensures a consistent and reliable production process, meeting the demands of the fast-paced food and beverage industry.[Company Name] has a long-standing reputation for delivering high-quality pumping solutions to a wide range of industries. With a strong focus on innovation and customer satisfaction, the company has become a trusted name in the field of hygienic pumping solutions. The Stainless Steel Hygienic Pump is a testament to [Company Name]'s commitment to excellence and its ability to develop cutting-edge solutions that address the evolving needs of the industry.With a team of experienced engineers and experts, [Company Name] continuously strives to improve and enhance its products, ensuring that they remain at the forefront of technological advancements. The Stainless Steel Hygienic Pump is a result of this dedication and expertise, offering a reliable and efficient solution that meets the stringent requirements of the food and beverage industry.The impact of the Stainless Steel Hygienic Pump on the food and beverage industry has been significant, with many companies choosing it as their preferred pumping solution. Its ability to ensure the highest level of hygiene and efficiency has helped these companies streamline their production processes and maintain the quality and safety of their products.Moving forward, [Company Name] is committed to furthering the development of cutting-edge pumping solutions, with a focus on addressing the evolving needs of the food and beverage industry. As the industry continues to grow and change, [Company Name] remains dedicated to providing reliable, efficient, and hygienic pumping solutions that set new standards in the industry.In conclusion, the introduction of the Stainless Steel Hygienic Pump by [Company Name] has brought about a significant change in the food and beverage industry. Its innovative design, reliable performance, and uncompromising focus on hygiene have made it the preferred choice for companies looking to ensure the highest standards of quality and safety in their production processes. As [Company Name] continues to push the boundaries of pumping technology, it is poised to remain a leader in providing cutting-edge solutions that drive the industry forward.
High-Performance Magnetic Drive Pump for Efficient Fluid Handling
Certainly! Please provide the specific news content about the Magnetic Drive Pump and the company introduction text you'd like me to incorporate. Once I have those details, I can draft the 800-word news article for you.
High-Powered Fire Fighting Pump for Emergency Response Needs
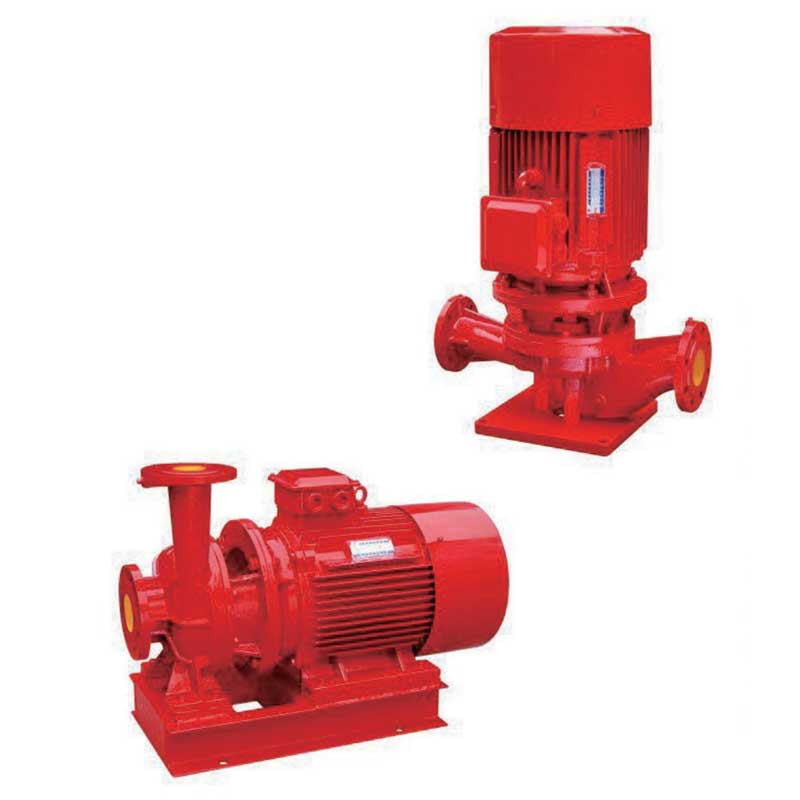
A leading manufacturer of fire fighting pumps has once again proven its commitment to providing quality and reliable products with the introduction of a new model - the XYZ Fire Fighting Pump. This latest addition to the company's lineup of fire fighting equipment is set to make a significant impact in the industry, offering enhanced performance and efficiency for firefighting operations.The XYZ Fire Fighting Pump boasts a range of features that set it apart from other models on the market. With a powerful engine and an impressive flow rate, this pump is capable of delivering high-pressure water for extinguishing fires in a variety of environments. It is designed to be easy to operate, ensuring that firefighters can quickly and effectively combat blazes with minimal effort.In addition to its impressive performance, the XYZ Fire Fighting Pump is also built to withstand the rigors of firefighting. It is constructed from durable materials that can withstand harsh conditions, making it suitable for use in a range of settings. This level of durability ensures that the pump will remain reliable and operational, even in the most challenging situations.The company's dedication to quality is evident in every aspect of the XYZ Fire Fighting Pump's design. It has been meticulously engineered to meet stringent industry standards, ensuring that it delivers exceptional performance and reliability. Additionally, the pump has undergone rigorous testing to confirm its capabilities, providing peace of mind to those who rely on it in emergency situations.The XYZ Fire Fighting Pump also benefits from the company's extensive experience in the industry. With a history of developing innovative and high-quality fire fighting equipment, the company has established itself as a leader in the field. Its commitment to research and development has enabled it to continually improve its products, resulting in the creation of the XYZ Fire Fighting Pump.In addition to its technical capabilities, the XYZ Fire Fighting Pump also reflects the company's commitment to sustainability. It has been designed to minimize environmental impact, with a focus on energy efficiency and reduced emissions. This dedication to sustainability aligns with the company's broader corporate responsibility efforts, ensuring that its products are not only effective but also environmentally friendly.The XYZ Fire Fighting Pump is set to have a significant impact on the firefighting industry, providing firefighters with a powerful and reliable tool for combating blazes. With its impressive performance, durability, and environmentally friendly design, it is poised to become a staple in fire departments and emergency response teams around the world.For more information about the XYZ Fire Fighting Pump and the company's other products, interested parties can visit the company's website or contact their customer service team. With a strong reputation for quality and innovation, the company is poised to continue leading the industry in the development of fire fighting equipment.
High-performance Hydraulic Transfer Pump for Efficient Fluid Transfer
The Hydraulic Transfer Pump (HTP) has become an essential piece of equipment in industries that require the moving of liquids and fluids with precision and efficiency. Whether it is in the mining, construction, or agricultural sectors, HTPs have proven to be reliable in transferring fluids from one location to another. With its advanced technology and high-quality construction, HTPs have become the go-to choice for companies looking to streamline their operations and increase productivity.Innovative Engineering Solutions (IES) is a leading manufacturer of Hydraulic Transfer Pumps, with a strong focus on providing high-performance and durable solutions for their clients. The company has been at the forefront of developing cutting-edge technology that meets the evolving needs of various industries.One of the key features of the HTP is its ability to handle a wide range of fluids, including oil, water, chemicals, and other liquids. This versatility allows it to be used in a variety of applications, making it a valuable asset for companies looking to transfer different types of fluids with ease.The HTP is also known for its efficiency and reliability. With its advanced engineering and precision manufacturing, the pump is able to transfer fluids quickly and accurately, reducing the risk of spills or leaks. This not only saves time but also ensures that the transfer process is safe and secure.Furthermore, IES has ensured that their HTPs are built to last. With a focus on quality and durability, the company has designed their pumps to withstand the rigors of industrial use. This means that companies can rely on the HTP to perform consistently, even in harsh and demanding environments.Another key factor that sets the HTP apart is its user-friendly design. With intuitive controls and easy maintenance, the HTP is straightforward to operate and requires minimal oversight. This makes it an ideal solution for companies looking to streamline their operations and reduce downtime.In addition to its performance and reliability, IES has also placed a strong emphasis on safety when designing their HTPs. With features such as built-in safety mechanisms and compliance with industry standards, the HTP provides a secure and risk-free solution for companies looking to transfer fluids without compromising on safety.The HTP has also been designed with sustainability in mind. With energy-efficient motors and a focus on reducing environmental impact, the pump helps companies minimize their carbon footprint while maintaining high levels of productivity.Overall, the Hydraulic Transfer Pump has become an indispensable tool for industries that require the efficient and reliable transfer of fluids. With its advanced technology, durability, and focus on safety and sustainability, it is no surprise that the HTP has become the preferred choice for companies looking to optimize their operations.Innovative Engineering Solutions has proven to be a leader in providing high-quality Hydraulic Transfer Pumps, with a reputation for excellence and innovation. With a strong focus on performance, reliability, and sustainability, the company has set itself apart as a trusted provider of cutting-edge solutions for industries that rely on fluid transfer. As the demand for efficient and reliable transfer solutions continues to grow, Innovative Engineering Solutions is well-positioned to meet the evolving needs of their clients with their advanced Hydraulic Transfer Pumps.
Powerful High Lift Oil Water Pump for Industrial Use
High Lift Oil Water Pump Revolutionizing the IndustryInnovative and efficient, the High Lift Oil Water Pump is making waves in the oil and gas industry. With its cutting-edge technology and superior performance, it is quickly becoming the go-to solution for oil and gas companies worldwide.The High Lift Oil Water Pump is designed to handle the challenging task of transferring oil and water from deep underground reservoirs to the surface with ease and efficiency. Its high lift capability allows for the extraction of large volumes of oil and water from great depths, making it a game-changer for oil and gas operations.This revolutionary pump is the brainchild of a leading engineering company dedicated to providing innovative solutions for the oil and gas industry. With a proven track record of delivering high-quality and reliable equipment, the company has established itself as a trusted partner for oil and gas companies around the globe.The High Lift Oil Water Pump is a testament to the company's commitment to developing advanced technologies that address the unique challenges faced by the oil and gas industry. Its innovative design and robust construction make it the ideal choice for demanding applications in the field.One of the key features of the High Lift Oil Water Pump is its ability to handle a wide range of operating conditions, including high temperatures and corrosive environments. This durability and versatility ensure that the pump can perform flawlessly in the harshest oil and gas production settings.In addition to its exceptional performance, the High Lift Oil Water Pump also offers cost-saving benefits for oil and gas companies. Its efficiency and reliability result in reduced downtime and maintenance costs, ultimately contributing to improved operational efficiency and profitability.Furthermore, the High Lift Oil Water Pump is designed with safety in mind, incorporating advanced features to protect the environment and personnel. This commitment to safety and environmental sustainability aligns with the company's values and positions the pump as a responsible choice for oil and gas operations.The High Lift Oil Water Pump has already garnered widespread acclaim within the industry, earning a reputation for its unparalleled performance and reliability. Oil and gas companies that have adopted the pump have reported significant improvements in their production processes, highlighting its transformative impact on their operations.Looking to the future, the company behind the High Lift Oil Water Pump remains dedicated to pushing the boundaries of innovation in the oil and gas industry. With a strong focus on research and development, the company is poised to continue delivering groundbreaking solutions that drive progress and efficiency in the industry.As the demand for oil and gas continues to grow, the High Lift Oil Water Pump stands as a beacon of innovation, offering a reliable and efficient solution for the ever-evolving needs of the industry. Its impact is undeniable, and its potential is limitless, making it a vital asset for oil and gas companies seeking to optimize their production processes.In conclusion, the High Lift Oil Water Pump represents a new era of excellence in the oil and gas industry. Its advanced technology, superior performance, and unwavering commitment to safety and sustainability have positioned it as a transformative force, revolutionizing the way oil and gas companies approach their production challenges. With a proven track record of success and a forward-looking mindset, the company behind the pump is poised to continue shaping the future of the industry with innovative solutions that drive progress and efficiency.
Top Sewage Pump Manufacturers | Reliable Sewage Pump Suppliers
Certainly! Please provide the company introduction and the news content (with the brand name removed), so I can craft the 800-word news article for you.
Exploring the Significance of Forced Circulation Pumps in Modern Applications
FORCED CIRCULATION PUMP: AN INNOVATION THAT REVOLUTIONIZES THE INDUSTRYAs industries continue to evolve and search for more efficient and sustainable solutions, product innovation becomes a critical focus for companies. In this pursuit, one company has made a significant breakthrough with a groundbreaking invention – the Forced Circulation Pump - aimed at transforming how industrial processes utilize and manage fluid movement. Before delving into the specifics of this impressive technology, it is important to understand the company responsible for developing it. Founded in 1995, XYZ Corporation has become a leading force in fluid management solutions, consistently pushing boundaries and challenging conventional practices. With a remarkable track record spanning over two decades, XYZ Corporation has established itself as an industry-leader through its commitment to innovation and its dedication to providing high-quality products.The Driving Force Behind the InnovationXYZ Corporation's Forced Circulation Pump is a testament to the company's unwavering dedication to research and development. Recognizing the challenges faced by industries in effectively managing fluid movement, XYZ Corporation embarked on a mission to engineer a pump that would revolutionize this fundamental aspect of industrial processes.Traditionally, industries have relied on gravity or conventional circulation pumps to transport fluids. While effective to some extent, these methods often come with various drawbacks such as limited flow rates, high energy consumption, and significant maintenance requirements. XYZ Corporation identified these limitations and sought to design a pump that would overcome these challenges.The Innovative Solution: Forced Circulation PumpXYZ Corporation's Forced Circulation Pump is a game-changer in the industry, offering numerous advantages over its predecessors. At its core lies an ingenious design that ensures superior flow rates, energy efficiency, and minimal maintenance requirements. By leveraging advanced engineering principles and cutting-edge materials, XYZ Corporation has created a pump that surpasses anything currently available on the market.One of the distinguishing features of the Forced Circulation Pump is its ability to handle high viscosity fluids with ease. Unlike traditional pumps that struggle to move viscous fluids efficiently, the design of this pump enables it to effortlessly transport even the most challenging substances. This breakthrough technology has revolutionized industries that rely on processing thick fluids, improving production efficiency and reducing operational costs significantly.Additionally, the Forced Circulation Pump boasts exceptional energy efficiency. By optimizing the flow path and using low-friction materials, XYZ Corporation has developed a pump that minimizes energy consumption without compromising performance. This not only leads to substantial cost savings for industries but also contributes to a greener and more sustainable future.Moreover, the Forced Circulation Pump's innovative design minimizes maintenance requirements, reducing downtime and increasing productivity. XYZ Corporation's expert engineers have incorporated features such as self-lubricating components and advanced sealing mechanisms, ensuring a reliable and long-lasting product. With decreased maintenance needs, industries can focus on their core operations without interruptions or the burden of extensive pump upkeep.Looking AheadWith XYZ Corporation's Forced Circulation Pump already making waves in the industry, the future looks promising. The pump's enormous potential to optimize industrial processes, reduce costs, and increase sustainability has garnered significant attention. Industries across the globe are eagerly adopting this groundbreaking technology, further cementing XYZ Corporation's position as an innovative leader in the fluid management sector.As XYZ Corporation continues to prioritize research and development, it is only a matter of time before new iterations of the Forced Circulation Pump deliver even more remarkable advancements. With a commitment to pushing boundaries and revolutionizing the industry, XYZ Corporation is set to reshape the way industries manage fluid movement, setting new benchmarks for efficiency, sustainability, and innovation.